Project overview
Railway signaling equipment
Relay enclosure
To be supplied from real project data
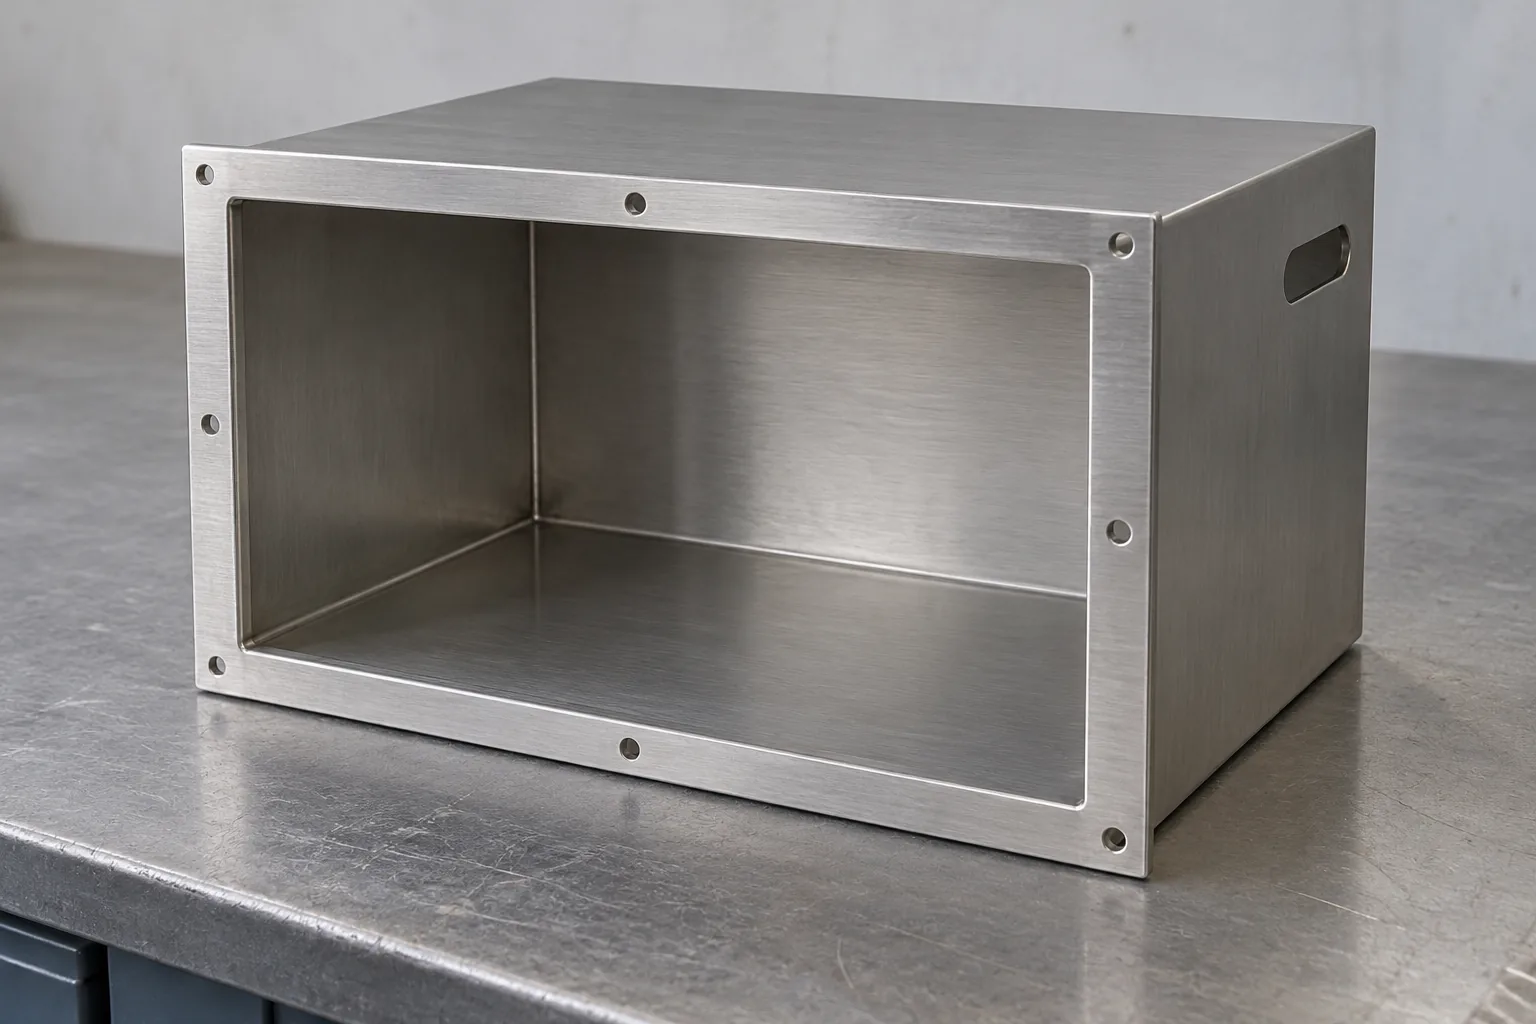
A railway signaling relay enclosure made from 304 stainless steel by sheet metal fabrication, focused on bend stack-up and gasket-flange coplanarity
What this case documents—and what it does not
Public evidence
No project documentation was supplied; the railway application, enclosure, 304 stainless steel, sheet metal process, and stated challenge are planning premises
Confirm from customer files
Installation environment, sheet gauge, cutouts, bend radii, weld details, gasket interface, finish, tolerances, quantity, inspection plan, and results—To be supplied from real project data
The specified sector, component, material, process, and challenge are topic premises only. All other exact facts not provided must be labeled To be supplied from real project data, with public, customer-file, and prohibited categories clearly separated
Engineering focus
Bend-stack datum strategy—show how feature references and bend order influence door, panel, and internal mounting relationships
Gasket-flange coplanarity—explain how tooling contact, corner design, handling, and localized correction affect the sealing interface
Joining distortion management—connect tack sequence, heat input, and inspection checkpoints without prescribing unverified production parameters
Application and planning basis
The proposed enclosure houses relay or control assemblies behind a gasketed opening; its flange must support the mating panel.
No publicly verified project facts were supplied. The table separates topic premises from missing customer-file data; prohibited claims remain excluded below.
| Parameter | Value / evidence status |
|---|---|
| Product | Railway signaling relay enclosure — planning premise |
| Service | Sheet metal fabrication — planning premise |
| Process | Cutting, bending and joining — planning premise |
| Material | 304 stainless steel — planning premise |
| Stage, gauge, dimensions, bend radii, finish | To be supplied from real project data |
| Weld specification, tolerance, roughness, quantity, protection requirement | To be supplied from real project data |
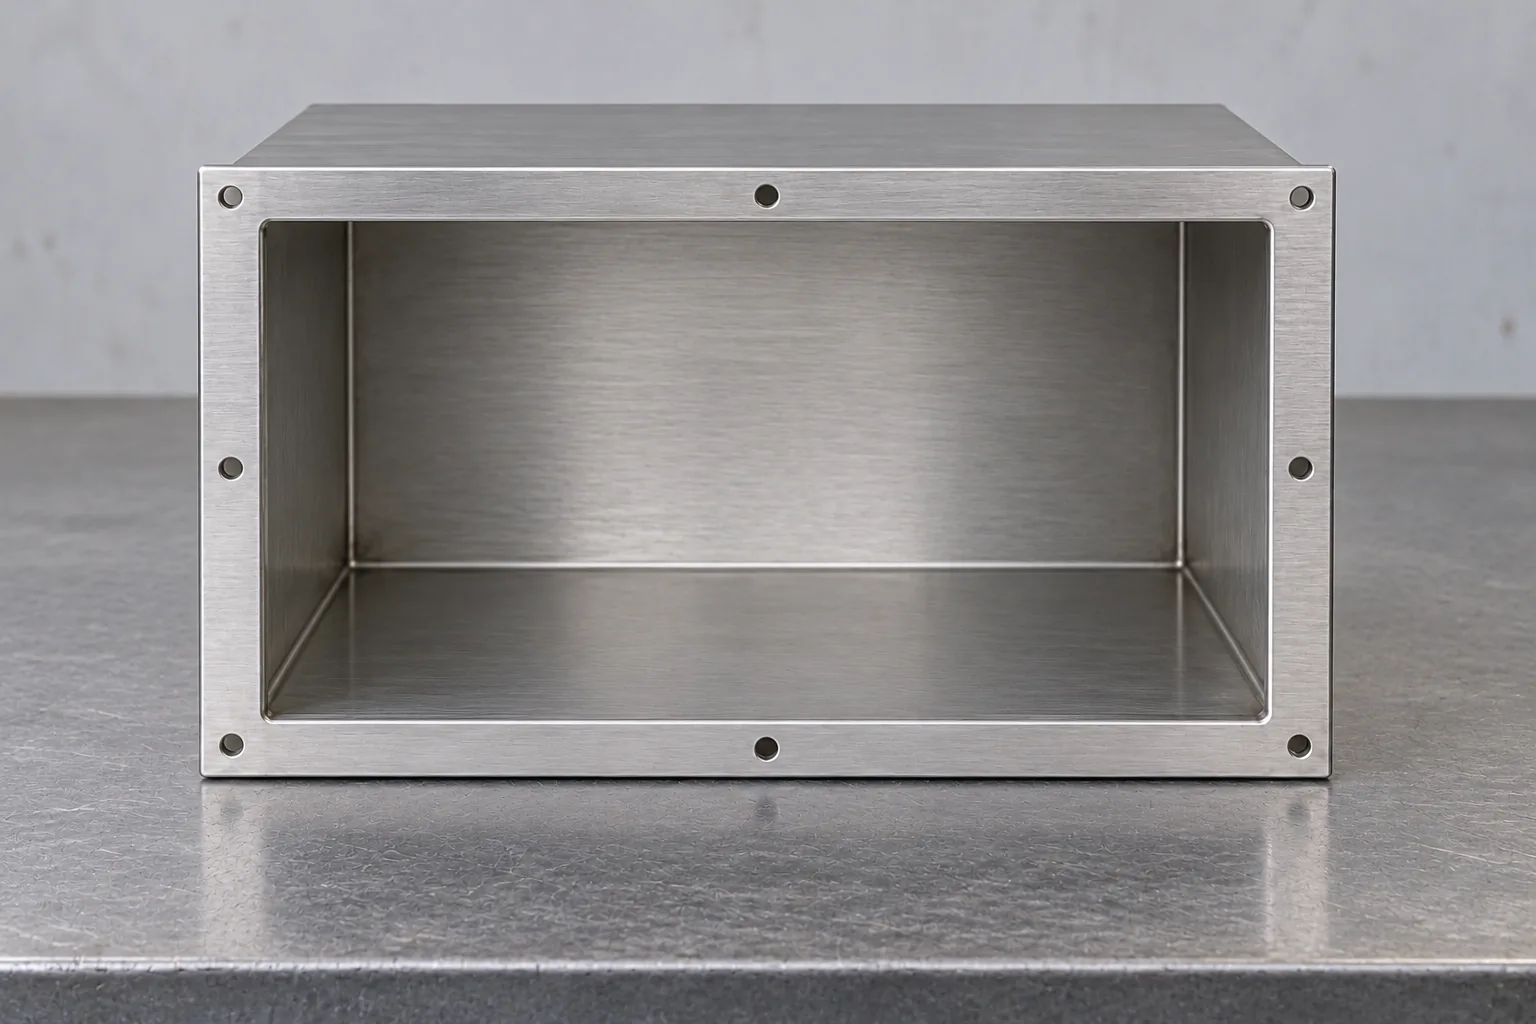
Preserve references as bends accumulate
Bend allowances and shifted references can displace later features, accumulating error in the opening and mounting pattern.
Validate the flat pattern against the intended stock, tooling and bend geometry. Keep assembly references accessible through the bend sequence.
Mismatch before joining directs investigation toward blank geometry, forming and datums. Change after joining warrants reviewing heat and restraint; timing alone does not prove cause.
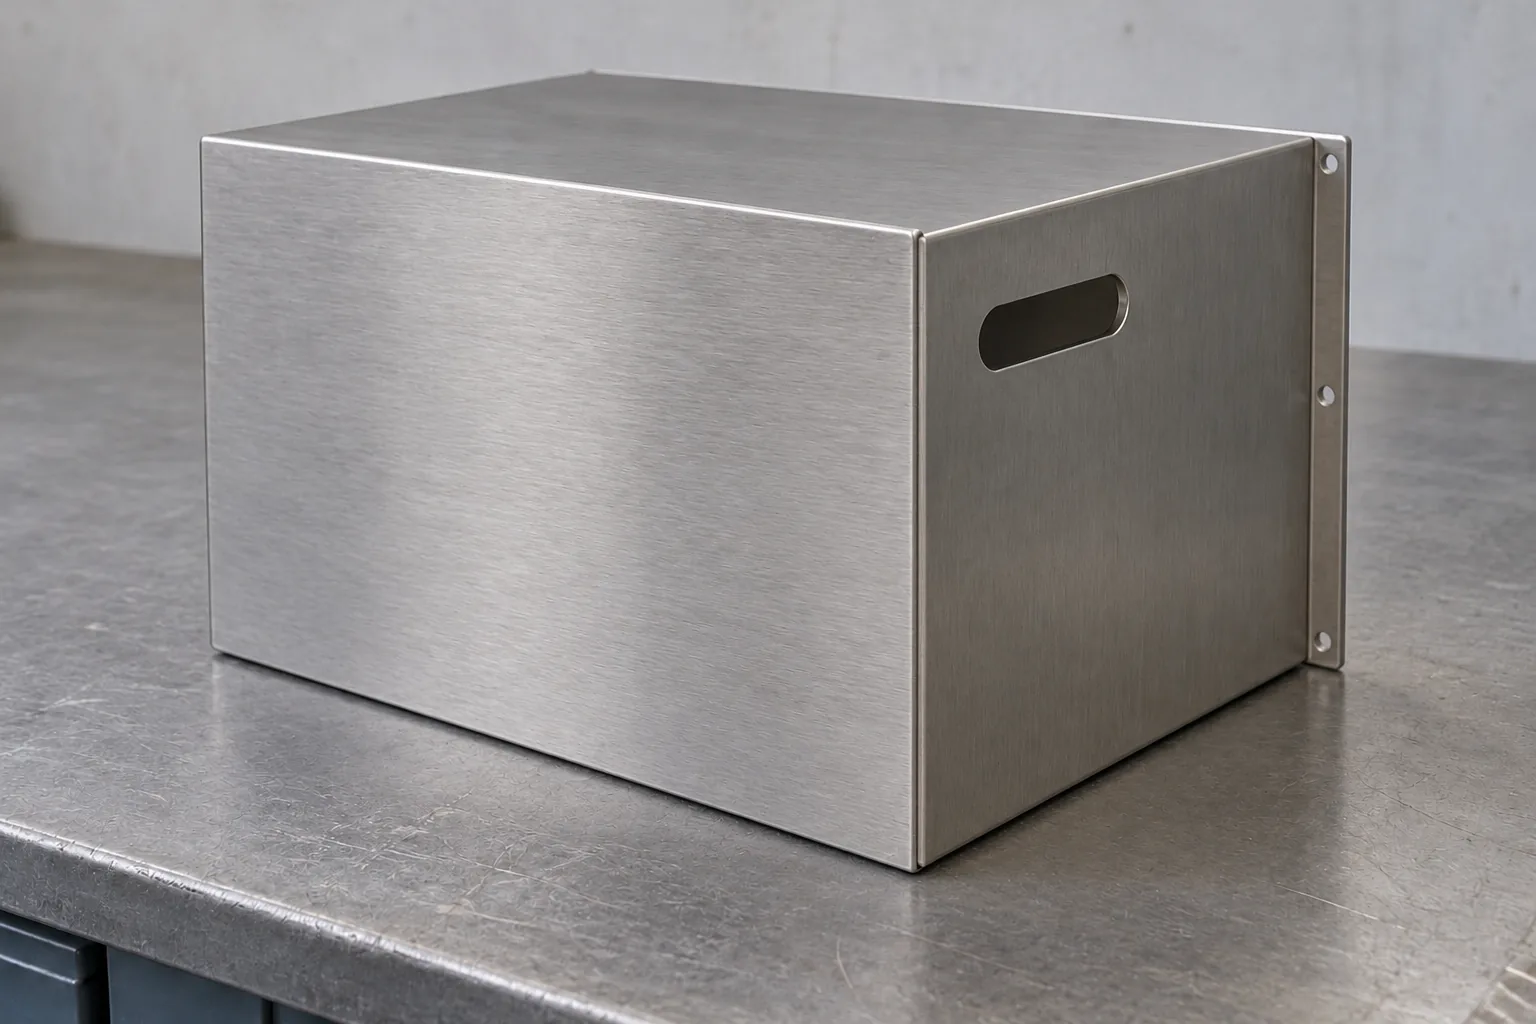
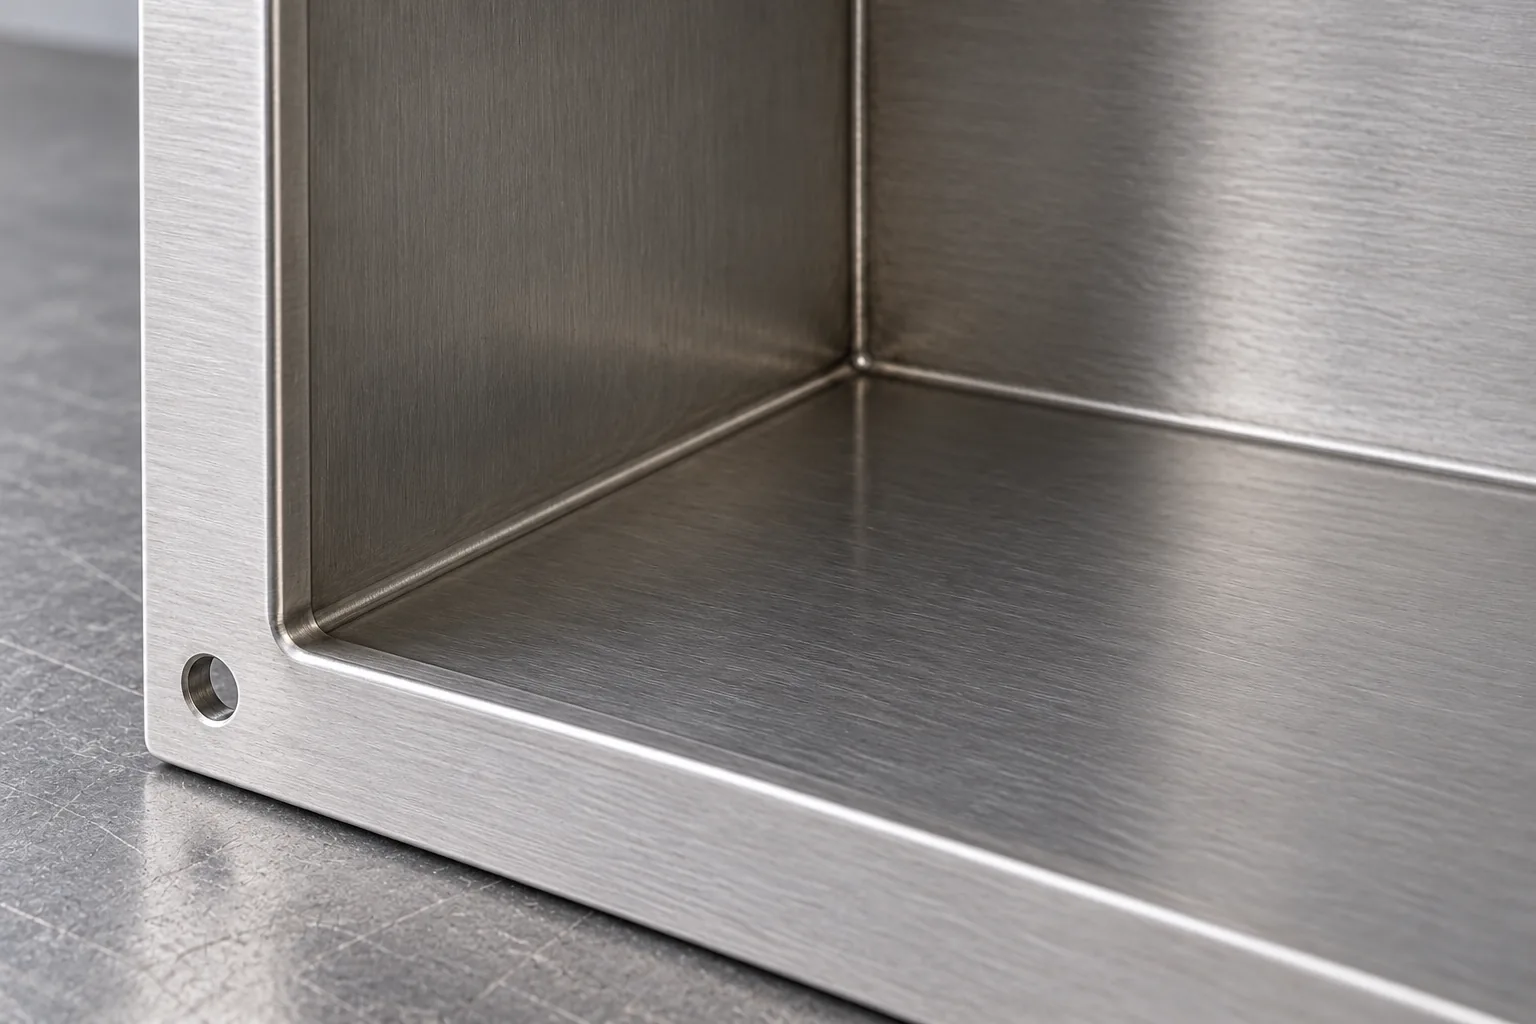
Support the flange without hiding its free shape
Coplanarity means contact surfaces share a plane. Tool contact, corner transitions or handling can tilt the flange; clamping may conceal its released shape.
Inspect under drawing-defined support conditions. Distinguish assembly restraint from free shape, and check nearby features before accepting localized correction.
Manage joining heat and restraint together
Heating and cooling move metal; joint geometry and restraint determine where movement appears. Corner joining can consequently pull the flange out of plane.
Coordinate the approved joining method, tack sequence and fixture. Compare restrained and released geometry; investigate changes before repeating the route.
A connected cutting, forming and joining route
Preserve assembly references at each handover.
- Review CAD, drawings, gasket interface and evidence status.
- Validate allowances, cutouts and applicable grain direction.
- Cut and deburr without damaging contact surfaces.
- Form bends while preserving the governing references.
- Fixture and join to the approved specification; monitor movement.
- Finish, clean and inspect flange, opening and mounting relationships.
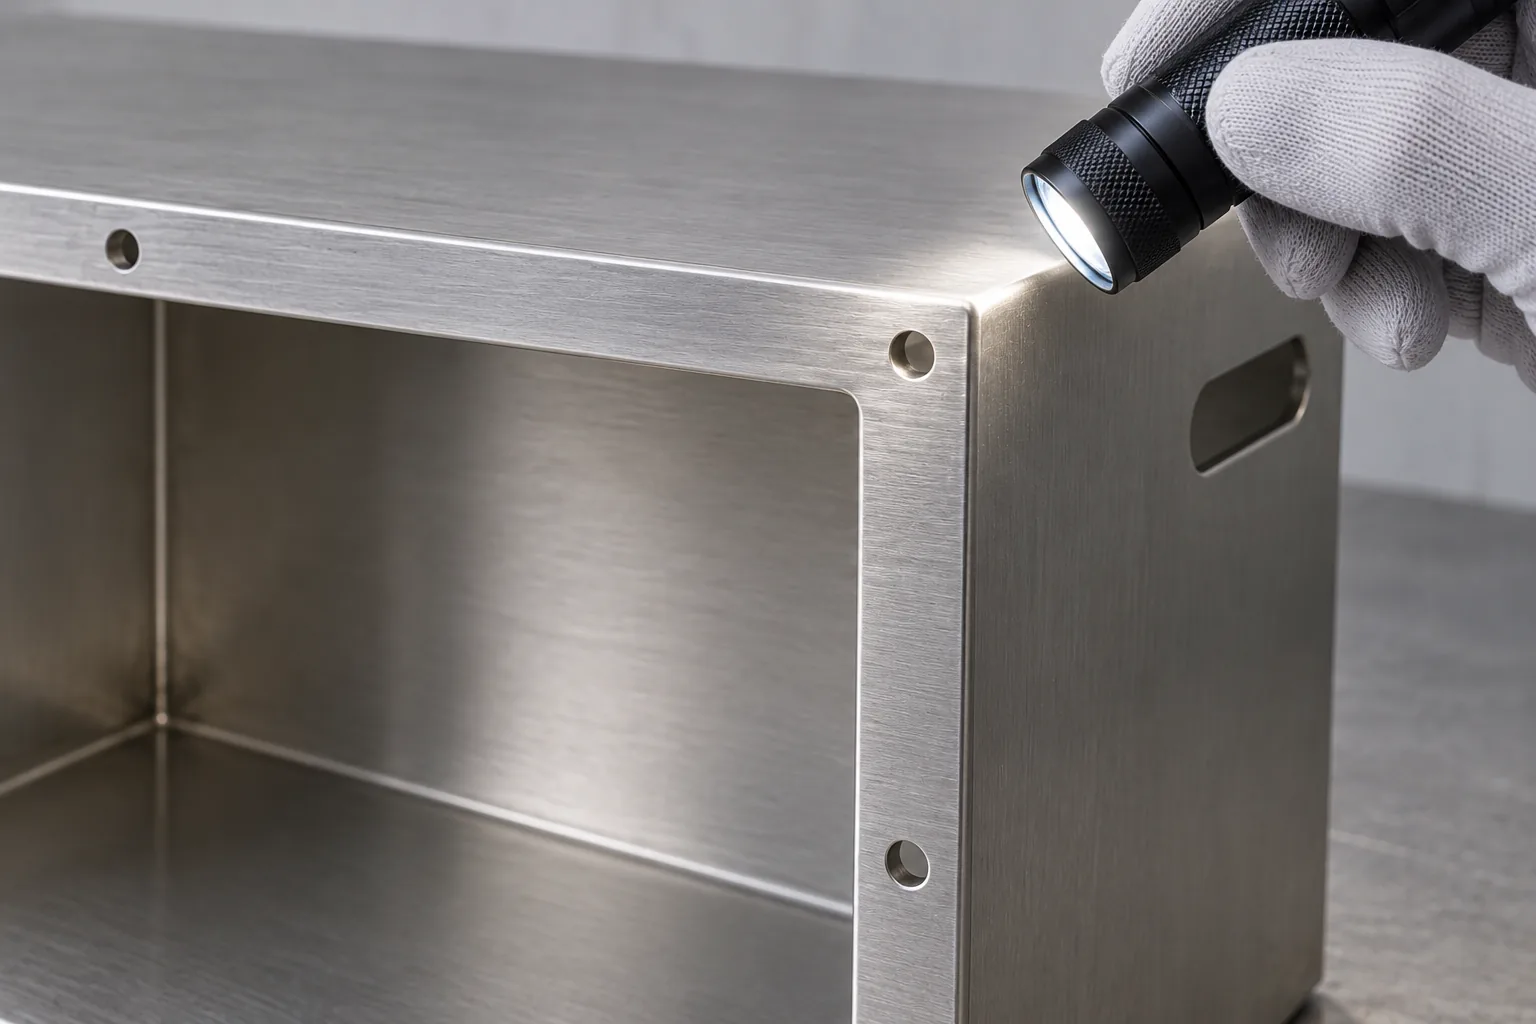
Verify feature relationships, then test the assembly
Compare stages using consistent references and support. If dimensions pass but assembly does not, check the panel, gasket and fastening conditions against acceptance requirements; assess environmental performance through applicable testing.
| Feature | Control intent | Typical verification |
|---|---|---|
| Gasket flange | Contact-plane geometry | Surface comparison in the agreed support condition |
| Door or opening | Panel relationship | Drawing inspection and authorized assembly check |
| Mounting holes | Datum-relative position | Coordinate or template inspection |
| Joined corners | Movement and joint condition | Stage comparisons and specified joint inspection |
| Edges | Burrs and damage | Visual and required edge checks |
Process planning
- 1. Review CAD, drawing, gasket interface, and evidence status. 2. Validate flat pattern, bend deductions, cutouts, and grain direction where applicable. 3. Cut and deburr the blank. 4. Form bends in a datum-preserving sequence. 5. Fixture and join corners using the approved specification. 6. Finish, clean, and inspect flange, openings, and mounting relationships
Quality control
| Feature / control / verification |
|---|
| Use a Feature | Control Intent | Typical Verification table for the gasket flange, door/opening relationship, mounting holes, joined corners, and edges |
| discuss suitable dimensional and visual methods but withhold unsupplied readings and environmental-test results |
Prepare your RFQ
3D model, flat or formed drawing, sheet grade and gauge, bend radii, joining standard, gasket definition, cutout and mounting tolerances, finish, quantity, inspection requirements, packaging, and target lead time
Documented outcome and verification boundary
Report only customer-approved dimensional, assembly, and test evidence. Do not infer sealing performance, railway compliance, corrosion life, or production acceptance from geometry alone
Guaranteed ingress protection, railway certification, distortion-free welding, universal bend accuracy, perfect fit, fixed corrosion life, price, or lead time
Prepare the RFQ and define an evidence-backed outcome
Supply model and drawings, stock and bend details, joining and gasket requirements, tolerances, finish, quantity, inspection scope, environment, packaging and delivery needs. These define fabrication and quotation scope.
Outcome records are To be supplied from real project data. Publish only customer-approved dimensional, assembly and test evidence. Reassess each comparable project's gasket, environment and drawing before transferring a route. Upload drawings to resolve interface questions, then configure a quote around the agreed scope.
Frequently asked questions
Why can a trial enclosure fit while a later batch needs adjustment?
Check stock, setup and restraint variation before treating a trial fit as evidence of repeatability.
Can tightening the panel compensate for an uneven gasket flange?
Extra load may distort parts or compress the gasket unevenly. Evaluate specified assembly loading rather than compensating blindly.
Does specifying 304 stainless steel settle suitability for the installation?
Review exposure, finish and maintenance with evidence appropriate to the installation; the grade alone does not settle suitability.
When should the gasket supplier participate in fabrication planning?
Involve the supplier before finalizing contact geometry, assembly loading and test criteria, particularly where those requirements remain unclear.
What makes an inspection report useful for investigating flange movement?
Record drawing revision, datums, support and fabrication stage so process changes can be distinguished from measurement changes.