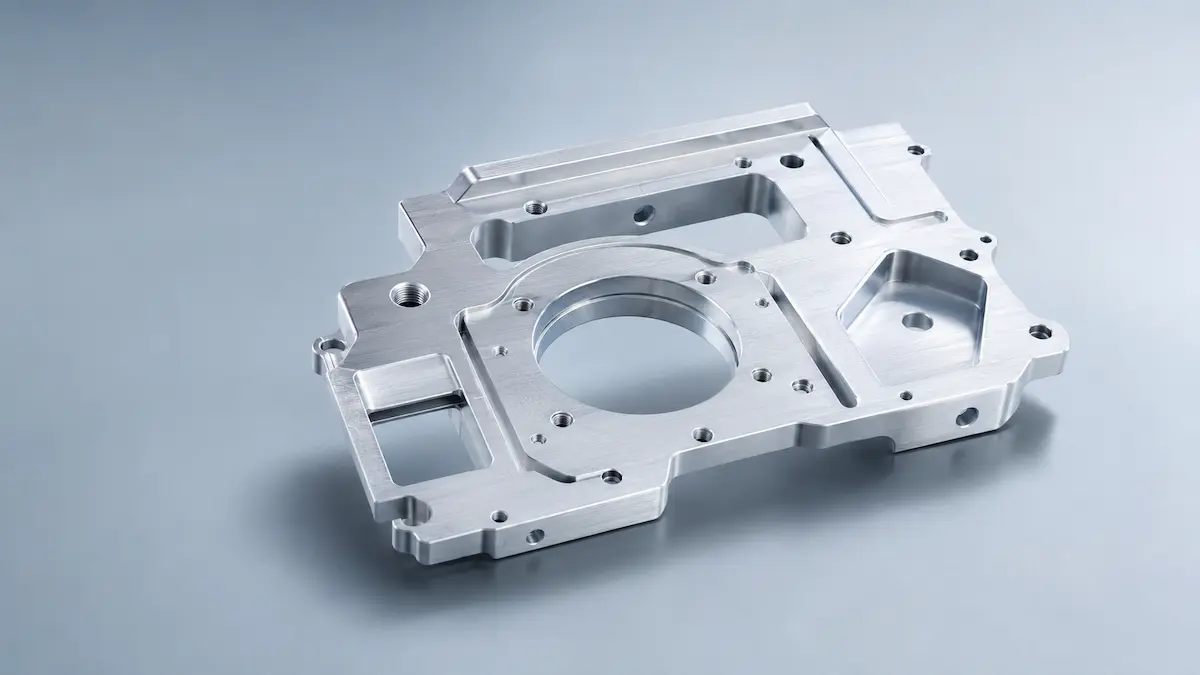
Post-processing options
Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.
Remove burrsDeburring is used to improve the appearance of parts, assembly, or functional verification effects, and it is necessary to confirm the impact on dimensions, strength, and delivery in combination with material characteristics.
ChamferChamfering is used to improve the appearance of parts, assembly, or functional verification effects, and the dimensions, strength, and delivery impact need to be confirmed in combination with material characteristics.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
BrushedBrushing is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
AnodizingSuitable for aluminum alloy appearance and protective treatment, pay attention to the impact of film thickness on hole position and assembly surface.
Hard oxidationHard oxidation is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
Powder sprayingSuitable for metal surface protection and color consistency; when coatings are thick, assembly gaps must be reserved.
Key control point
Size impactAL5052 is suitable for sandblasting oxidation; Drawing oxidation; powder spraying and painting; But the bending position; Cut edges and welding positions affect the final appearance consistency; Anodizing changes the surface color and size; Powder and painting increase the coating thickness; Hole position
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.