Support Hours: 09:00–18:00 (GMT+8) · Messages and quote requests are accepted 24/7.
Material Database

Brass H59

Suitable for general hardware parts, decorative parts, small mechanical parts, joints, nuts, valve fittings, stamped parts, and low- to medium-strength copper alloy parts as a general-purpose Brass material.

Material description

Brass H59 is a commonly used copper-zinc alloy material with good strength, plasticity, wear resistance, corrosion resistance, and machinability. It has a relatively low copper content, and its material cost is usually lower than high-copper Brass such as H62 and H65. It is commonly used in hardware parts, decorative parts, joints, nuts, valve accessories, mechanical parts, stamped parts, and ordinary copper alloy components. Compared toPure CopperT2 and TU2 Oxygen-Free Copper, H59 has weaker electrical and thermal conductivity but better strength, hardness, and processing adaptability.

H59BrassBrass H59Ordinary BrassCopper-zinc alloy59BrassH59 copperBrass Stick H59Brass plate H59Copper alloy H59
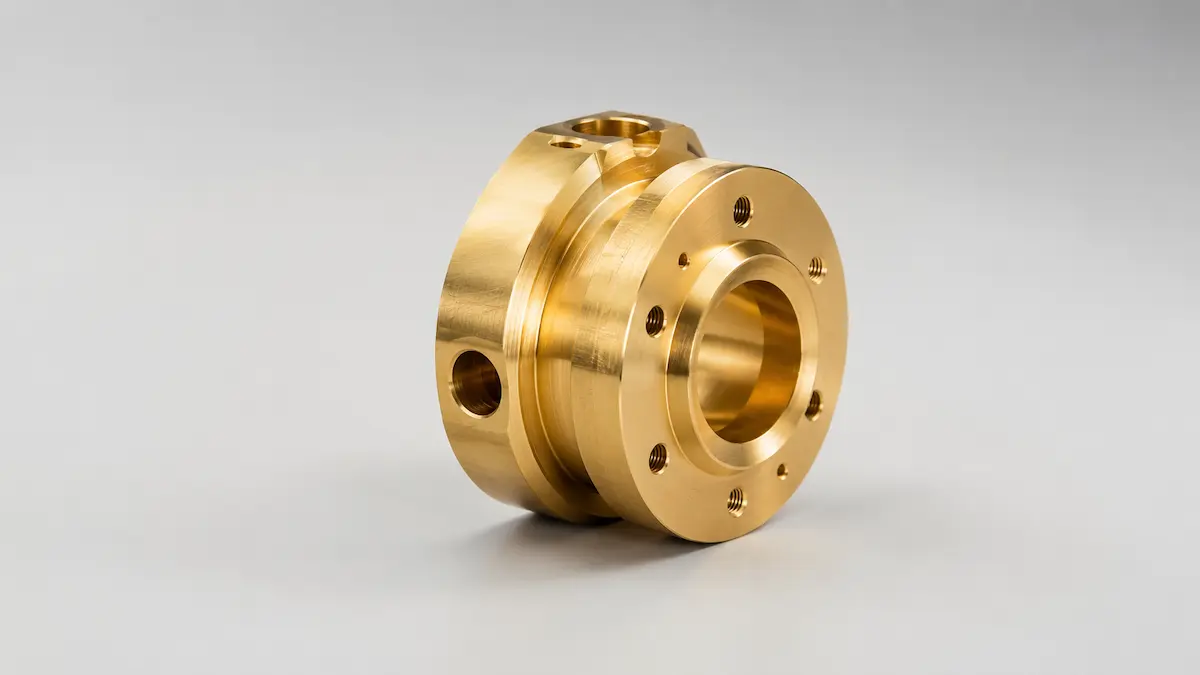
Brass H59 has good mechanical strength and general processing performanceIts color is golden yellow or BrassSuitable for making decorative parts and ordinary hardware functional partsIt is harder thanPure CopperIt is more suitable for turning and machining structural partsHowever, its electrical and thermal conductivity is inferior to pure copper materialsH59 has better corrosion resistance than ordinary carbon steelBut it's humidSalt sprayAcidity and alkalis
Brass H59
CNC MachiningMetals

Material compatibility assessment

By focusing on application scenarios, boundaries of advantages, and non-recommended scenarios, it helps sales, customer service, and quoting staff quickly determine whether the material meets current part requirements.

Core advantages

It has relatively low cost, good strength, hardness higher thanPure Copper, good machinability, good wear resistance, a distinct golden yellow texture on the surface, suitable for turning, milling, drilling, and tapping, as well as for hardware and decorative parts processing.

Suitable for the product

Hardware accessories, decorative parts, nuts, studs, joints, valve accessories, plumbing parts, shaft sleeves, sleeves, gaskets, nameplates, keychains, instrument and meter parts, small mechanical parts, stamped parts, bent parts, ordinary copper alloy structural parts, and small-batch Brass processed parts.

Not suitable for the product

High conductivity copper busbars, high thermal conductivity heat dissipation components, high elasticity clips, high-strength load-bearing structural parts, high wear-resistant heavy-duty sliding parts, direct contact parts with food, medical implant parts, strong acid and strong alkali environmental parts, long-term seawater contact parts, products with strict environmental requirements for lead-free materials, electronic components requiring the highest conductivity.

Key parameter references

The following parameters come from product information and material knowledge fields, used for design review, quotation communication, and preliminary judgment before material selection.

Material positioningSuitable for general hardware parts, decorative parts, small mechanical parts, joints, nuts, valve fittings, stamped parts, and low- to medium-strength copper alloy parts as a general-purpose Brass material.
Precision performanceBrass H59 is suitable for CNC turning, milling, drilling, tapping, stamping, bending, and general precision machining. Compared toPure Copper, H59 is less likely to stick during machining and offers better machining stability; Compared to HPb59-1, H59 has slightly weaker machinability, but is more suitable for scenarios where lead-containing materials are not desired. Actual accuracy is affected by part dimensions, cutting tools, clamping methods, machining paths, material conditions, and post-processing methods.
Dimensional tolerancesThe standard dimensional tolerances for CNC machining Brass H59 can be referenced ± 0.02mm to ±0.10mm, while ordinary structural parts and turned parts can be evaluated at ±0.05mm to ±0.20mm. Stamping, bending, and large thin sheets may have larger overall dimensional tolerances. These values are standard reference ranges and are not absolute guaranteed tolerances for all structures. Precision shaft diameter, threads, hole positions, and mating surfaces should be separately marked with tolerance requirements.
Minimum Wall ThicknessThe wall thickness of ordinary CNC machined structures is recommended to be no less than 0.8mm-1.0mm. Small turned parts, sleeves, and decorative parts can be further optimized according to the structure, but it is not recommended to make large areas too thin. Threaded connections, press-in parts, thin-walled sleeves, and load-bearing positions should be appropriately thickened to avoid processing deformation, compression cracking, or insufficient assembly strength.
Recommended wall thicknessFor ordinary small Brass, it is recommended to be above 1.0mm-2.0mm; the positions of nuts, joints, sleeves, decorative parts, and threaded holes should be appropriately thickened according to thread specifications, assembly force, and force requirements; For stamped or bent parts, it is recommended to determine wall thickness based on plate thickness, bending radius, and forming risk.
Minimum apertureCNC drilling can achieve smaller diameters, but deep small hole machining still requires consideration of chip removal, burrs, and tool strength. For general designs, the recommended aperture is no less than 0.8mm-1.0mm. Deep holes, small threaded holes, blind holes, and precision fit holes should be evaluated based on tool length, chip removal, burr control, and post-processing requirements.
Assembly clearanceFor precision metal assembly, 0.02mm-0.10mm per side can be reserved according to fitting requirements; for ordinary plug-ins, shaft hole fits, and hardware assembly, it is recommended to reserve 0.10mm-0.30mm per side. If subsequent nickel, chrome, tin, gold, or oxidation treatments are needed, additional gaps should be reserved according to the thickness of the coating. Press-in and knurled parts should be individually designed according to the fitting material, hole diameter, and indentation force.
Detailed performanceBrass H59 suitable for processing threads, chamfers, steps, holes, grooves, knurling, decorative textures, and small hardware details. After turning and milling, the details are rendered well, making it suitable for creating decorative structures with a metallic texture. For fine text, logos, and markings, it is recommended to achieve laser marking, engraving, etching, embossing, or electroplating to avoid designing complex textures that are difficult to process on overly small parts.
Surface effectBrass H59 raw surface usually appears as a golden yellow or Brass metallic texture. After turning and milling, a brighter metalworking surface is obtained; after polishing, a brighter Brass appearance is achieved; brushing produces a linear metallic texture; and after sandblasting, a matte Brass effect is achieved. Long-term exposure to air, humidity, or sweat environments may oxidize and darken, resulting in dark yellow, brown, or spots on the surface. If long-term appearance is needed, nickel, chrome, gold, transparent protection, or oxidation resistance treatments can be applied.

Typical application scenarios

Based on material characteristics and suitable product ranges, customer needs are broken down into easier application directions to determine.

Product validation

Hardware accessories, decorative parts, nuts, studs, joints, valve accessories, plumbing parts, shaft sleeves, sleeves, gaskets, nameplates, keychains, instrument and meter parts, small mechanical parts, stamped parts, bent parts, ordinary copper alloy structural parts, and small-batch Brass processed parts.

Reasons for material selection

Suitable for general hardware parts, decorative parts, small mechanical parts, joints, nuts, valve fittings, stamped parts, and low- to medium-strength copper alloy parts as a general-purpose Brass material.

Material characteristics

Brass H59 has good mechanical strength and general processing performance, with a color of golden yellow or Brass, suitable for making decorative parts and ordinary hardware functional parts. It is harder thanPure Copperand better suited for turning and machining structural parts, but its electrical and thermal conductivity is inferior to pure copper materials. H59 has better corrosion resistance than ordinary carbon steel, but it may oxidize, discolor, or corrode in humid conditions, salt spray, acids and alkalis, ammonia, or strongly corrosive environments.

Design and risk review

Based on wall thickness, hole position, assembly clearance, dimensional tolerances, and material usage risks, determine in advance whether the part structure is suitable for Brass H59.

Design considerations

  • When designing Brass H59 parts
  • It should be combined with its strength
  • Machinability and appearance characteristics in the design
  • Threads
  • Hole position
  • The knurling and assembly positions should ensure sufficient wall thickness and machining space
  • For exterior parts, consider the polishing direction
  • Brushing direction and subsequent oxidation treatment
Precision performanceBrass H59 is suitable for CNC turning, milling, drilling, tapping, stamping, bending, and general precision machining. Compared toPure Copper, H59 is less likely to stick during machining and offers better machining stability; Compared to HPb59-1, H59 has slightly weaker machinability, but is more suitable for scenarios where lead-containing materials are not desired. Actual accuracy is affected by part dimensions, cutting tools, clamping methods, machining paths, material conditions, and post-processing methods.
Dimensional tolerancesThe standard dimensional tolerances for CNC machining Brass H59 can be referenced ± 0.02mm to ±0.10mm, while ordinary structural parts and turned parts can be evaluated at ±0.05mm to ±0.20mm. Stamping, bending, and large thin sheets may have larger overall dimensional tolerances. These values are standard reference ranges and are not absolute guaranteed tolerances for all structures. Precision shaft diameter, threads, hole positions, and mating surfaces should be separately marked with tolerance requirements.
Quality riskThe main risks Brass H59 include surface oxidation discoloration, batch color differences, processing burrs, thread slippage, insufficient corrosion resistance, and environmental compliance risks. It is suitable for ordinary Brass hardware and decorative parts, but not for high conductivity, high thermal conductivity, high elasticity, or severe corrosion scenarios. For long-term appearance parts or in humid environments, focus should be paid to surface protection, plating quality, oxidation resistance, and usage environment.
Surface effectBrass H59 raw surface usually appears as a golden yellow or Brass metallic texture. After turning and milling, a brighter metalworking surface is obtained; after polishing, a brighter Brass appearance is achieved; brushing produces a linear metallic texture; and after sandblasting, a matte Brass effect is achieved. Long-term exposure to air, humidity, or sweat environments may oxidize and darken, resulting in dark yellow, brown, or spots on the surface. If long-term appearance is needed, nickel, chrome, gold, transparent protection, or oxidation resistance treatments can be applied.

Post-processing and assembly precautions

Post-processing of Brass H59 affects appearance, dimensions, hole position, assembly clearance, and usage validation results, and should be explained in advance during quotation, DFM review, and sample confirmation stages.

Post-processing options

Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.

Remove burrsDeburring is used to improve the appearance of parts, assembly, or functional verification effects, and it is necessary to confirm the impact on dimensions, strength, and delivery in combination with material characteristics.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
PolishingUsed to improve transparency or surface smoothness, may change edge details and local dimensions.
BrushedBrushing is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
Nickel platingNickel plating is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties with dimensions, strength, and delivery impact.
Chrome platingChrome plating is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
tin-platedTin plating is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties to confirm dimensions, strength, and delivery impact.

Key control point

Size impactBrass H59 burrs are likely to form after processing; Oil stains and surface oxidation; Timely cleaning and protection are required; Polishing; Brushing and sandblasting alter surface conditions and local dimensions; Electroplating increases surface thickness and affects assembly clearances; When used as exterior parts; Scratches should be controlled
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.

Structure and usage boundaries

For common issues such as threads, snaps, strength, temperature resistance, and weather resistance, identify in advance whether the material needs to be replaced or if another processing method should be used.

Thread Recommendation

Applicable ScopeBrass H59 can be tapped, thread turned, and rolled, making it suitable for making ordinary nuts, joints, and copper alloy fasteners.
Risk pointSince Brass strength is lower than steel parts, high locking force, frequent disassembly and assembly, or heavy load locations require careful design. It is recommended to increase thread engagement length, enlarge thread specifications, or switch to steel or stainless steel parts.
Recommended practiceAvoid walls near threaded holes that are too thin to prevent cracking or thread slipping during assembly.

Buckle recommendation

Applicable ScopeBrass H59 is not suitable for designing large-deformation elastic buckles like plastics, nor for long-term high-frequency elastic structures.
Risk pointMetal slots, limit steps, threaded locking, pin connections, press-inserts, or low-deformation engagement structures can be designed.
Recommended practiceIf spring clips, spring plates, or highly elastic conductive clips are needed, elastic materials such as beryllium copper, phosphor bronze, 65Mn, or 301 stainless steel should be considered.

Strength and Environment

Mechanical strengthBrass H59 has certain strength and hardness, higher thanPure CopperT2 and TU2 Oxygen-Free Copper, making it more suitable for ordinary hardware, threaded parts, joints, and decorative structural components.
Environmental boundaryHowever, it is not a high-strength structural material and is not suitable to replace steel parts, stainless steel, or high-strength copper alloys for heavy-duty structures.
Recommended practiceThe load-bearing structure should focus on wall thickness, thread meshing length, hole edge distance, assembly force, and operating load. Brass H59 temperature resistance is superior to plastics and some low-temperature materials, making it suitable for general metal engineering environments. However, material strength, surface condition, and coating properties may change at high temperatures, requiring careful evaluation in long-term high-temperature or thermal cycling environments. When involving high-temperature, welding, near heat sources, or high-temperature assembly applications, verification should be conducted in consideration of specific temperature, load, surface treatment, and structural requirements. Brass H59 gradually oxidizes and darkens in air, and environments such as humidity, sweat, salt spray, acids and alkalis, sulfides, or ammonia accelerate corrosion and discoloration. Ordinary indoor hardware can be improved for stability through cleaning, nickel plating, chrome plating, gold plating, tin plating, or oxidation resistance. If customers need to use H59 for extended periods outdoors, drinking water, food contact, or high corrosion resistance, they should use H59 with caution and prioritize stainless steel, lead-free eco-friendly Brass, or other corrosion-resistant materials.

Alternative material selection and final judgment

When customer demand exceeds Brass H59 material boundaries, it is necessary to combine strength, temperature resistance, toughness, long-term stability, and mass production goals to promptly recommend alternative materials or processing technologies.

Alternative material suggestions

If better ductility and processing stability are required, H62Brass can be chosen; If better machinability is required, HPb59-1 lead Brass can be chosen; If higher electrical and thermal conductivity is required, Pure CopperT2 or TU2 Oxygen-Free Copper can be chosen; If higher elasticity and fatigue life are needed, beryllium copper C17200 or phosphor bronze can be chosen; If higher corrosion resistance is required,304 Stainless Steel, 316, or QAl9-4 Aluminum Bronze can be chosen.

Material selection suggestions

If customers mainly care about Brass appearance, ordinary mechanical strength, lower costs, and conventional hardware processing, Brass H59 is a more suitable choice. If customers require high-efficiency turning and batch processing of complex small hardware, consider HPb59-1; If customers have requirements for lead-free environmental protection, food contact, drinking water, or export regulations, they should confirm material standards in advance and, if necessary, choose lead-free Brass or other environmentally friendly materials.

Already have the blueprints? Directly enter the quotation for custom parts

After uploading 3D/2D drawings and supplementing materials, quantities, tolerances, surface treatments, and delivery requirements, XPartsLab will provide next steps in 3D printing manufacturability, cost, and delivery pathways.