Support Hours: 09:00–18:00 (GMT+8) · Messages and quote requests are accepted 24/7.
Material Database

T10 Carbon Steel

Carbon tool steel material suitable for making ordinary cutting tools, cutting tools, small cold work molds, wear-resistant parts, and tool parts requiring higher hardness and better edge retention.

Material description

T10 is a commonly used high-carbon tool steel. After quenching and tempering, it can achieve higher hardness, better wear resistance, and better edge retention. Compared to T7 and T8, T10 has higher hardness and wear resistance, but its toughness and impact resistance are relatively weaker. It is commonly used for ordinary cutting tools, cutting tools, blanking dies, small cold work tools, woodworking tools, measuring tools, wear-resistant parts, and tool parts that require high hardness.

T10 steelT10 carbon tool steelCarbon tool steel T10High carbon steel T10Tool steel T10Blade steelCold work tool steelOrdinary high-carbon tool steel
T10 steel is a high-carbon tool steelIts main feature is high hardness after heat treatmentGood wear resistanceStrong blade retentionSuitable for making at room temperatureLow speedTools used under light to medium load conditionsCutting tools and wear-resistant toolsCompared to the T7T8
T10 Carbon Steel
CNC MachiningMetals

Material compatibility assessment

By focusing on application scenarios, boundaries of advantages, and non-recommended scenarios, it helps sales, customer service, and quoting staff quickly determine whether the material meets current part requirements.

Core advantages

After heat treatment, it has high hardness, good wear resistance, good edge retention, lower cost than alloy tool steel, suitable for low-speed room temperature tools, small blanking and cutting tools, and can achieve high surface hardness through quenching and tempering.

Suitable for the product

Ordinary cutting tools, scissor blades, woodworking tools, low-speed cutting tools, punches, blanking molds, small cold work molds, scrapers, saw blades, measuring tools, templates, wear-resistant pads, positioning blocks, limit blocks, wear-resistant parts of ordinary fixtures, small cutting tools, and tool parts.

Not suitable for the product

High-speed cutting tools, high-temperature red-hardness requirements, high-impact heavy-duty parts, highly corrosive environment parts, long-term exposed outdoor parts, large-size high-hardenability parts, high-precision long-life molds, food direct contact parts, medical implant parts, and metal parts requiring rust-free maintenance.

Key parameter references

The following parameters come from product information and material knowledge fields, used for design review, quotation communication, and preliminary judgment before material selection.

Material positioningCarbon tool steel material suitable for making ordinary cutting tools, cutting tools, small cold work molds, wear-resistant parts, and tool parts requiring higher hardness and better edge retention.
Precision performanceT10 steel is suitable for CNC machining, wire cutting, grinding, drilling, tapping, and finishing after heat treatment. In the annealed state, machinability is relatively good; after quenching, hardness increases, making machining significantly more difficult, usually requiring grinding, electrical machining, or wire cutting to complete key dimensions. Actual accuracy is affected by machining methods, heat treatment deformation, part thickness, cutting edge structure, and post-processing methods.
Dimensional tolerancesFor CNC machining of T10 steel, the standard dimensional tolerances can be evaluated as ± 0.02mm to ±0.10mm, while ordinary structural parts can be evaluated at ± 0.10mm to ±0.20mm; If parts require quenching, tempering, or surface treatment, dimensional changes or deformation may occur after heat treatment. It is recommended to heat treat key dimensions before finishing or grinding. This value is a standard reference range and does not guarantee absolute tolerances for all structures.
Minimum Wall ThicknessThe wall thickness of ordinary CNC machined structures is recommended to be no less than 0.8mm-1.0mm. Areas requiring quenching, cutting edges, impact resistance, or as wear-resistant structures should be appropriately thickened. Thin walls, sharp thin edges, slender structures, and complex cross-sections are prone to deformation, cracking, or edge chipping during heat treatment.
Recommended wall thicknessFor ordinary small tools and wear-resistant parts, it is recommended to be above 1.5mm-3.0mm; for punches, insert bodies, cutting edges, mold parts, and positions bearing local loads, it is recommended to be above 2.0mm, and design should be based on heat treatment deformation and grinding allowance. The cutting edge area needs to balance sharpness, support thickness, and crack resistance.
Minimum apertureCNC machining can achieve smaller hole diameters, but the hole size and roundness may change after quenching. For general designs, the recommended aperture is no less than 1.0mm. It is recommended to reserve machining allowance for precision holes, positioning holes, pin holes, and threaded holes. If necessary, heat treatment should be followed before drilling, reaming, grinding, or wire cutting refinishing.
Assembly clearanceFor ordinary metal assembly, it is recommended to reserve 0.10mm-0.30mm on one side; precision fit positions should be individually determined according to heat treatment and grinding processes. If parts require heat treatment, blackening, phosphating, electroplating, or rust prevention, heat treatment deformation and surface treatment thickness should be considered to avoid over-tightening or surface scratches.
Detailed performanceT10 steel is suitable for machining holes, grooves, steps, chamfers, cutting edges, punch profiles, positioning surfaces, and wear-resistant structural details. Before heat treatment, CNC machining and wire cutting details perform well; after heat treatment, grinding can improve the quality of key surfaces and cutting edges. Fine text, logos, and markings are recommended to be achieved through laser marking, engraving, or etching; it is not recommended to design complex decorative details in areas with high-hardness thin blades.
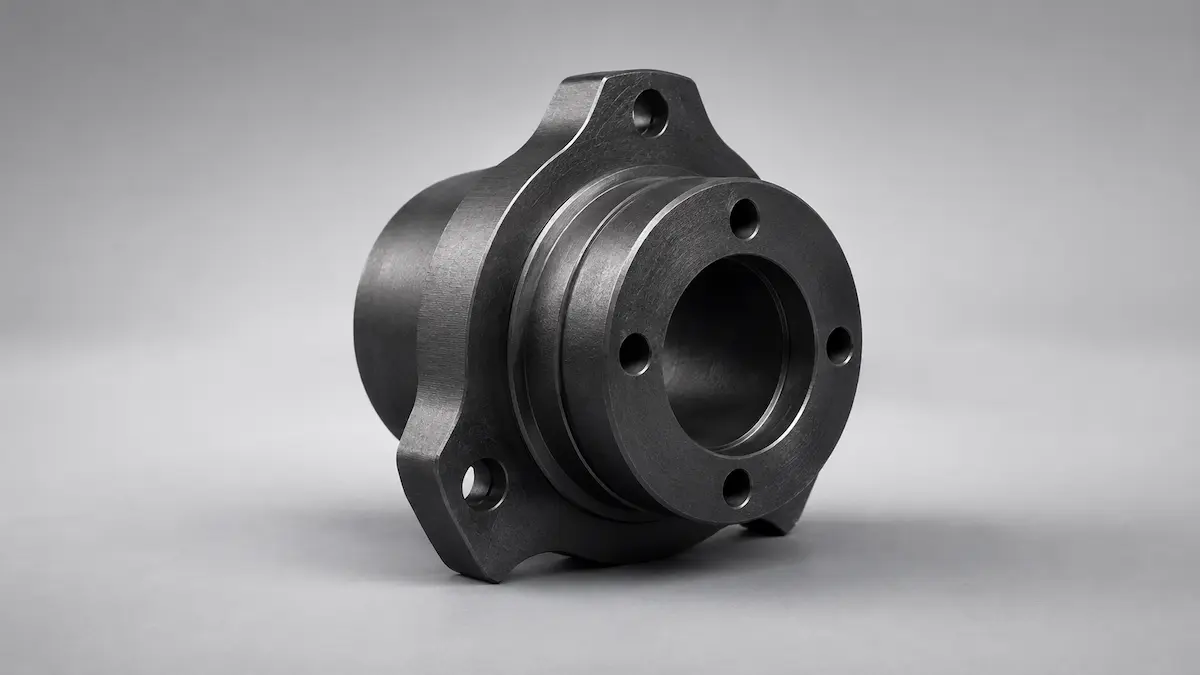
Surface effectThe original processed surface of T10 steel is usually silver-gray or gray-black metallic surface. After heat treatment, oxidation, blackening, decarburization layers, or surface marks may appear. After grinding and polishing, a relatively smooth metal surface is obtained; after blackening or phosphating, a black or gray-black rust-resistant appearance is achieved. If long-term appearance stability is desired, rust prevention treatment or replacement with stainless steel materials is required.

Typical application scenarios

Based on material characteristics and suitable product ranges, customer needs are broken down into easier application directions to determine.

Product validation

Ordinary cutting tools, scissor blades, woodworking tools, low-speed cutting tools, punches, blanking molds, small cold work molds, scrapers, saw blades, measuring tools, templates, wear-resistant pads, positioning blocks, limit blocks, wear-resistant parts of ordinary fixtures, small cutting tools, and tool parts.

Reasons for material selection

Carbon tool steel material suitable for making ordinary cutting tools, cutting tools, small cold work molds, wear-resistant parts, and tool parts requiring higher hardness and better edge retention.

Material characteristics

T10 steel is a high-carbon carbon tool steel, characterized mainly by high hardness after heat treatment, good wear resistance, and strong edge retention. It is suitable for making tools, cutting tools, and wear-resistant tools used under normal temperature, low speed, and light to medium load conditions. Compared to T7 and T8, T10 is harder and more wear-resistant, but has weaker toughness and is more prone to cracking under impact or when the structure is too thin. Its hardenability, red hardness, and corrosion resistance are limited, making it unsuitable as a substitute for high-speed steel, alloy tool steel, or stainless tool steel.

Design and risk review

Based on wall thickness, hole position, assembly clearance, dimensional tolerances, and material usage risks, determine in advance whether the part structure is suitable for T10.

Design considerations

  • When designing T10 steel parts,
  • Heat treatment feasibility should be prioritized
  • Blade support
  • Direction of force
  • Stress concentration and post-processing allowance
  • Sharp angle
  • Thin blade at the base
  • At the edge of the hole and at abrupt cross-sectional changes, fillets or transition structures should be added
Precision performanceT10 steel is suitable for CNC machining, wire cutting, grinding, drilling, tapping, and finishing after heat treatment. In the annealed state, machinability is relatively good; after quenching, hardness increases, making machining significantly more difficult, usually requiring grinding, electrical machining, or wire cutting to complete key dimensions. Actual accuracy is affected by machining methods, heat treatment deformation, part thickness, cutting edge structure, and post-processing methods.
Dimensional tolerancesFor CNC machining of T10 steel, the standard dimensional tolerances can be evaluated as ± 0.02mm to ±0.10mm, while ordinary structural parts can be evaluated at ± 0.10mm to ±0.20mm; If parts require quenching, tempering, or surface treatment, dimensional changes or deformation may occur after heat treatment. It is recommended to heat treat key dimensions before finishing or grinding. This value is a standard reference range and does not guarantee absolute tolerances for all structures.
Quality riskThe main risks of T10 steel include heat treatment deformation, quenching cracking, edge chipping, insufficient toughness, surface decarburization, uneven hardness, poor corrosion resistance, and long-term exposed rust. It is suitable for ordinary cutting tools and wear-resistant tools, but not suitable for strong impact, high precision, high corrosion resistance, high temperature, high speed, or heavy-duty working conditions. When involving cutting edges, sharp corners, thin walls, hole edges, and abrupt cross-sectional structures, focus should be placed on controlling fillets, heat treatment processes, hardness requirements, and post-processing allowances.
Surface effectThe original processed surface of T10 steel is usually silver-gray or gray-black metallic surface. After heat treatment, oxidation, blackening, decarburization layers, or surface marks may appear. After grinding and polishing, a relatively smooth metal surface is obtained; after blackening or phosphating, a black or gray-black rust-resistant appearance is achieved. If long-term appearance stability is desired, rust prevention treatment or replacement with stainless steel materials is required.

Post-processing and assembly precautions

Post-processing of T10 affects appearance, dimensions, hole position, assembly clearance, and usage validation results, and should be explained in advance during quotation, DFM review, and sample confirmation stages.

Post-processing options

Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.

Remove burrsDeburring is used to improve the appearance of parts, assembly, or functional verification effects, and it is necessary to confirm the impact on dimensions, strength, and delivery in combination with material characteristics.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
PolishingUsed to improve transparency or surface smoothness, may change edge details and local dimensions.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
Annealing fireAnnealing is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties with dimensions, strength, and delivery impact.
NormalNormalizing is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
QuenchingQuenching is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
TemperingTempering is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.

Key control point

Size impactT10 steel typically requires quenching and tempering to achieve target hardness and wear resistance; Deformation may occur during heat treatment; Cracking; Decarbonization; Uneven hardness or cracking of the cutting edge; Precision dimensions; Blade edge; It is recommended to reserve allowance for grinding or finishing after heat treatment at the hole position and assembly surface
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.

Structure and usage boundaries

For common issues such as threads, snaps, strength, temperature resistance, and weather resistance, identify in advance whether the material needs to be replaced or if another processing method should be used.

Thread Recommendation

Applicable ScopeT10 steel can be threaded, but after high-hardness heat treatment, tapping becomes more difficult and prone to tool wear, chipping, or thread damage.
Risk pointIt is recommended to complete thread bottom holes and rough machining before heat treatment, and key threads should be finely trimmed as needed after heat treatment.
Recommended practiceFor frequent disassembly or high locking force positions, sufficient thread engagement length should be ensured, and the structure of the screw sleeve or standard fastener should be considered.

Buckle recommendation

Applicable ScopeT10 steel is not suitable for designing large deformation elastic buckles like plastics, nor for structures that undergo long-term repeated elastic deformation.
Risk pointMetal slots, positioning blocks, pressure plates, limiting parts, pin connections, or screw fixing structures can be designed.
Recommended practiceIf spring clips, spring plates, or high-elasticity clips are needed, 65Mn, 301 stainless steel, spring steel, or specialized elastic materials should be chosen.

Strength and Environment

Mechanical strengthAfter appropriate quenching and tempering, T10 steel has high hardness, good wear resistance, and good edge retention, making it suitable for ordinary tools, cutting tools, punches, and small wear-resistant parts.
Environmental boundaryCompared to T7 and T8, it has better hardness and wear resistance;
Recommended practiceHowever, their toughness and impact resistance are relatively weaker. Actual performance heavily depends on heat treatment processes, hardness control, cross-sectional dimensions, and operating conditions. T10 steel is not classified as a high-temperature tool steel; it performs well at room temperature and at low speeds, but its hardness and edge retention ability decrease at high temperatures. It is not suitable for high-speed cutting, high-temperature friction, or long-term high-temperature load-bearing scenarios. When involving high-temperature cutting tools, hot-work molds, or high-temperature wear-resistant applications, high-speed steel, hot-work mold steel, or high-temperature alloy materials should be selected. T10 steel has poor weather resistance and is prone to rust in exposed environments, especially in humid conditions, salt spray, acids and alkalis, sweat, or outdoor environments. Tool parts should be kept dry after use and coated with anti-rust oil. For long-term storage, outdoor or humid environments, it is recommended to apply blackening, phosphating, electroplating, anti-rust oil, or other surface protection; If maintenance-free corrosion resistance is required, stainless steel, tool steel, or other corrosion-resistant materials should be used instead.

Alternative material selection and final judgment

When customer demand exceeds T10 material boundaries, it is necessary to combine strength, temperature resistance, toughness, long-term stability, and mass production goals to promptly recommend alternative materials or processing technologies.

Alternative material suggestions

If better toughness and impact resistance are needed, T7, T8, 45# steel, 40Cr, or 42CrMo can be selected; If higher hardness and wear resistance are required, T12, Cr12, Cr12MoV, or high-speed steel can be chosen; If better red hardness and high-speed cutting performance are required, high-speed steel can be chosen; If better corrosion resistance is required,420 Stainless Steel, 440C, or other stainless steel tool materials can be chosen; If it is just ordinary structural parts, you can choose Q235, 20# steel, or 45# steel.

Material selection suggestions

If customers need low-speed ambient temperature tools, ordinary blanking tools, small wear-resistant parts, or tool parts with certain requirements for maintaining the cutting edge, T10 is a more suitable and low-cost choice. If a part requires high impact toughness, high-temperature cutting, high-speed wear resistance, long-term corrosion resistance, or long-life precision molds, priority should be given to alloy tool steel, high-speed steel, mold steel, or stainless steel tool steel.

Already have the blueprints? Directly enter the quotation for custom parts

After uploading 3D/2D drawings and supplementing materials, quantities, tolerances, surface treatments, and delivery requirements, XPartsLab will provide next steps in 3D printing manufacturability, cost, and delivery pathways.