Support Hours: 09:00–18:00 (GMT+8) · Messages and quote requests are accepted 24/7.
Material Database

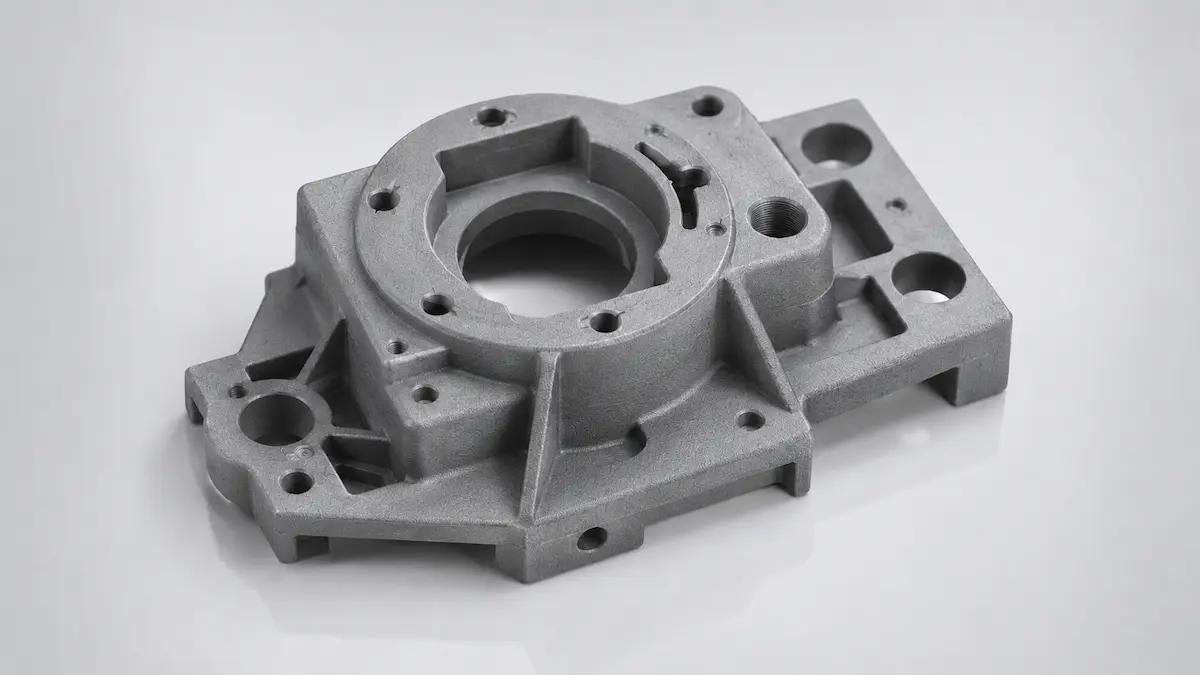
HP MJF Glass-Filled Nylon – Gray

Enhanced 3D printed nylon materials suitable for high-rigidity structural parts, dimensionally stable functional parts, fixtures and fixtures, small-batch engineering parts, and gray industrial samples.

Material description

HP MJF Glass-Filled Nylon – Gray is a reinforced nylon material commonly used in the HP Multi Jet Fusion process, typically based on nylon Nylon (PA)12 and with fiberglass or glass microbeads added as reinforcement fillers to improve the material's rigidity, dimensional stability, and heat resistance. Compared to ordinary nylon, HP MJF Glass-Filled Nylon – Gray is more suitable for making structural parts, brackets, fixtures, jigs, shell frameworks, and small-batch functional parts, but its toughness and elasticity are generally inferior to ordinary nylon.

HP nylon fiberglass grayHP Nylon FiberglassGray fiberglass nylonNylon (PA)12 fiberglass grayNylon (PA)12 GB grayGlass microbead reinforced nylonMJF gray reinforced nylon
HP MJF Glass-Filled Nylon – Gray is harder than ordinary nylon materialsMore stableIt is also less likely to cause obvious deformation due to stressSuitable for structural supportInstallation and positioningFixtures, fixtures, and engineering validationAfter reinforcing fiberglass or glass microbeadsImproved material rigidity and heat resistanceBut the material is toughElasticity and impact resistance may decrease
HP MJF Glass-Filled Nylon – Gray
3D PrintingPlastics

Material compatibility assessment

By focusing on application scenarios, boundaries of advantages, and non-recommended scenarios, it helps sales, customer service, and quoting staff quickly determine whether the material meets current part requirements.

Core advantages

High rigidity, good dimensional stability, better heat resistance than ordinary nylon, good wear resistance, suitable for functional component verification, suitable for complex structures, no need for traditional supports, suitable for small batch engineering parts, gray appearance facilitates observation of structural details and surface conditions.

Suitable for the product

Structural brackets, mounting seats, housing frameworks, fixtures and fixtures, functional prototypes, assembly verification parts, industrial equipment parts, robot structural parts, drone structural parts, automotive interior structural parts, electronic and electrical brackets, small batch functional parts, and engineering samples requiring high rigidity and dimensional stability.

Not suitable for the product

High-elasticity snap-fit parts, high-frequency bending parts, high-impact parts, transparent parts, high-gloss appearance parts, food direct contact parts, long-term heavy-duty load-bearing parts, high-strength parts replacing metals, transmission parts requiring extremely high precision, precision gears, and parts exposed for long-term outdoor use.

Key parameter references

The following parameters come from product information and material knowledge fields, used for design review, quotation communication, and preliminary judgment before material selection.

Material positioningEnhanced 3D printed nylon materials suitable for high-rigidity structural parts, dimensionally stable functional parts, fixtures and fixtures, small-batch engineering parts, and gray industrial samples.
Precision performanceHP MJF Glass-Filled Nylon – Gray usually have good dimensional stability, making them suitable for structural parts, assemblies, and functional verification parts. Actual accuracy is affected by equipment, material batches, part dimensions, placement direction, cooling and shrinkage, post-processing, and sandblasting and painting. Compared to ordinary nylon, reinforcement materials generally have a lower risk of deformation, but complex structures still require allowance for assembly.
Dimensional tolerancesStandard dimensional tolerances can refer to ± 0.20mm to ±0.40mm. This value is a reference value for conventional processes and does not guarantee the absolute tolerance of all structures. Large parts, thin-walled parts, elongated parts, complex structural parts, and post-processed parts may experience greater dimensional deviations. It is recommended to reserve margin for precision assembly positions, and if necessary, perform post-processing or trial assembly verification.
Minimum Wall ThicknessIt is recommended that the wall thickness be no less than 1.0mm. Small, non-stressed local structures can achieve about 0.8mm thickness, but are not recommended for large-area use. Due to the high rigidity of the material, it is recommended that the wall thickness of the load-bearing structure, screw connection position, and assembly position be no less than 1.5mm.
Recommended wall thicknessFor ordinary structural parts, 1.5mm-2.5mm is recommended; for clamps, brackets, mounting seats, and parts that need to withstand assembly forces, 2.0mm-3.0mm is recommended; for large-size thin-shell parts, adding ribs or locally thickening is recommended to improve rigidity and dimensional stability.
Minimum apertureIt is recommended that the aperture diameter be no less than 1.5mm. Small holes, deep holes, and curved channels tend to retain powder, making cleaning more difficult. It is recommended to reserve machining allowance for precision holes, screw holes, positioning holes, and assembly holes, and perform drilling, reaming, or post-tapping when necessary.
Assembly clearanceFor ordinary assembly, it is recommended to reserve 0.20mm-0.40mm on one side; for movable fits, 0.40mm-0.60mm should be reserved on one side. If sandblasting, sealing, painting, dyeing, or immersion treatments are needed later, an additional gap of about 0.10mm-0.20mm per side should be added.
Detailed performanceRaised text, fine textures, and decorative lines are recommended to be no less than 0.5mm-0.8mm. MJF nylon materials have a powdery granular texture on the surface, and their detail sharpness is not as sharp as photosensitive resin. Gray reinforced nylon is better suited for functional structural details, assembly positioning, and engineering marking, and is not suitable for ultra-fine exterior textures or high-precision decorative effects.
Surface effectThe original surface is usually gray or light gray, with a matte powder finish and a fine grainy texture. The gray surface is suitable for observing structural contours, edge details, and surface defects, and has strong engineering sample properties. After sandblasting, sealing, dyeing, or painting, color consistency and overall appearance can be improved, but it is difficult to directly achieve a high-gloss mirror finish.

Typical application scenarios

Based on material characteristics and suitable product ranges, customer needs are broken down into easier application directions to determine.

Product validation

Structural brackets, mounting seats, housing frameworks, fixtures and fixtures, functional prototypes, assembly verification parts, industrial equipment parts, robot structural parts, drone structural parts, automotive interior structural parts, electronic and electrical brackets, small batch functional parts, and engineering samples requiring high rigidity and dimensional stability.

Reasons for material selection

Enhanced 3D printed nylon materials suitable for high-rigidity structural parts, dimensionally stable functional parts, fixtures and fixtures, small-batch engineering parts, and gray industrial samples.

Material characteristics

HP MJF Glass-Filled Nylon – Gray is harder, more stable, and less prone to significant deformation under force compared to ordinary nylon materials, making it suitable for structural support, installation and positioning, fixtures and fixtures, and engineering verification. After reinforcing fiberglass or glass microbeads, material rigidity and heat resistance improve, but toughness, elasticity, and impact resistance may decrease, making it unsuitable for structures requiring frequent bending or high elastic deformation. The gray appearance is better suited for observing edge contours, assembly relationships, and surface details.

Design and risk review

Based on wall thickness, hole position, assembly clearance, dimensional tolerances, and material usage risks, we pre-judge whether the part structure is suitable for HP nylon & fiberglass gray.

Design considerations

  • It is recommended to avoid walls that are too thin during design
  • Sharp right angles
  • Overly long thin rods and large, thin planes without reinforcement
  • The load-bearing position should have rounded corners
  • Reinforcing ribs and transition structures
  • Screwed post
  • Installation holes and clamping positions should have sufficient wall thickness reserved
  • Locations requiring movable fitting should consider material rigidity and surface friction
Precision performanceHP MJF Glass-Filled Nylon – Gray usually have good dimensional stability, making them suitable for structural parts, assemblies, and functional verification parts. Actual accuracy is affected by equipment, material batches, part dimensions, placement direction, cooling and shrinkage, post-processing, and sandblasting and painting. Compared to ordinary nylon, reinforcement materials generally have a lower risk of deformation, but complex structures still require allowance for assembly.
Dimensional tolerancesStandard dimensional tolerances can refer to ± 0.20mm to ±0.40mm. This value is a reference value for conventional processes and does not guarantee the absolute tolerance of all structures. Large parts, thin-walled parts, elongated parts, complex structural parts, and post-processed parts may experience greater dimensional deviations. It is recommended to reserve margin for precision assembly positions, and if necessary, perform post-processing or trial assembly verification.
Quality riskThe main risk of HP MJF Glass-Filled Nylon – Gray is that customers easily mistake "glass fiber reinforcement" for being a substitute for metals or high-strength engineering plastics. Its rigidity and dimensional stability are better than ordinary nylon, but its toughness and impact resistance may not be better. Thin walls, sharp corners, snaps, elongated structures, threaded holes, and high-stress locations still require focused assessment of cracking, deformation, and assembly risks.
Surface effectThe original surface is usually gray or light gray, with a matte powder finish and a fine grainy texture. The gray surface is suitable for observing structural contours, edge details, and surface defects, and has strong engineering sample properties. After sandblasting, sealing, dyeing, or painting, color consistency and overall appearance can be improved, but it is difficult to directly achieve a high-gloss mirror finish.

Post-processing and assembly precautions

Post-processing of HP Nylon & Fiberglass - Gray affects appearance, dimensions, hole position, assembly clearance, and usage validation results, which need to be explained in advance during quotation, DFM review, and sample confirmation stages.

Post-processing options

Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.

Remove the powderDepowdering is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties with dimensions, strength, and delivery impact.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
DyeingSuitable for overall color treatment and appearance identification, with attention to color uniformity and material color absorption.
Seal the holeSealing holes are used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
Spray paintEnhances color and appearance consistency, but will increase coating thickness, so assembly surfaces need to allow for clearance.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
attacked YaSuitable for low-strength thread verification; the hole edge must ensure wall thickness; frequent disassembly or high-torque locking is not recommended.
Embedded nutsTo improve connection reliability, it is necessary to confirm the hole diameter, embedding depth, and surrounding material thickness in advance.

Key control point

Size impactHP nylon & fiberglass – gray surfaces usually have a fine grainy texture and powdery texture; Cleaning is needed before painting; Hole sealing and primer treatment; Otherwise, it may affect the adhesion of the paint surface; Glass fiber reinforced materials are relatively harder; During post-processing and tapping, attention should be paid to cracking or localized cracking at the hole edges; Gray surfaces are more likely to show powder residue than black ones; Stains and color differences
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.

Structure and usage boundaries

For common issues such as threads, snaps, strength, temperature resistance, and weather resistance, identify in advance whether the material needs to be replaced or if another processing method should be used.

Thread Recommendation

Applicable ScopeTapping or designing threads of larger sizes can be performed, but it is not recommended for high-strength frequent disassembly.
Risk pointFiberglass reinforced materials have high rigidity, and excessive stress at the thread positions may cause cracking or tooth stripping at the hole edges.
Recommended practiceFor reliable connection positions, it is recommended to use embedded nuts, metal sleeves, or post-processed threads. Add fillets and reinforcing ribs at the base of the screw post.

Buckle recommendation

Applicable ScopeHP MJF Glass-Filled Nylon – Gray not suitable for high-elasticity or high-frequency snap-fit structures.
Risk pointAfter glass fiber reinforcement, rigidity increases, but elasticity and toughness decrease, making clips more prone to breakage under excessive force.
Recommended practiceIf a latch must be designed, the fillet should be increased, the deformation stroke shortened, assembly stress reduced, and prioritized for low-frequency assembly verification.

Strength and Environment

Mechanical strengthHP MJF Glass-Filled Nylon – Gray has good rigidity, wear resistance, and structural support capabilities, making it suitable for brackets, mounting bases, fixtures, and engineering functional parts.
Environmental boundaryCompared to ordinary nylon, it is less prone to deformation, but its impact resistance and bending ability may not match that of unreinforced nylon.
Recommended practiceHigh-stress structures should focus on wall thickness, direction of load, hole edges, sharp corners, and threaded connection locations. Its temperature resistance generally surpasses that of ordinary nylon and photosensitive resins, making it suitable for structural verification in general engineering environments and at moderate temperatures. Specific temperature resistance depends on material type, glass fiber content, equipment processes, and post-processing. For applications involving long-term high temperatures or proximity to heat sources, supplier material data and actual tests should be used as the standard. It is not recommended to rely solely on "glass fiber reinforcement" to promise long-term high-temperature use. Nylon materials are exposed to long-term changes in ultraviolet rays, humidity, and temperature, which may cause moisture absorption, dimensional changes, yellowing, graying, or performance degradation. Gray looks dirtier and causes color differences than black, and long-term outdoor exposure may still cause aging. For outdoor or high-quality appearance scenarios, it is recommended to apply painting, hole sealing, or surface protection treatment.

Alternative material selection and final judgment

When customer demand exceeds the material boundaries of HP nylon & fiberglass-gray, it is necessary to combine strength, temperature resistance, toughness, long-term stability, and mass production goals to promptly recommend alternative materials or processing technologies.

Alternative material suggestions

If better toughness and impact resistance are needed, you can choose HP nylon Nylon (PA)12 gray, HP nylon Nylon (PA)12 black, or domestic nylon; If higher strength and temperature resistance are required, CNC aluminum alloy, CNC stainless steel, CNC Polyether Ether Ketone (PEEK), or CNC PPS can be chosen; If you need a better appearance, you can choose gray photosensitive resin, black photosensitive resin, or CNC ABS; If stronger wear resistance and precise motion performance are required, CNC Acetal (POM) is a good choice.

Material selection suggestions

If customers mainly care about rigidity, dimensional stability, structural support, installation positioning, and small batch functional parts, HP MJF Glass-Filled Nylon – Gray is a more suitable choice. If customers care more about toughness, snap elasticity, drop resistance, or frequent disassembly, they should prioritize ordinary nylon Nylon (PA)12 or materials with better toughness. If customers require a high-gloss appearance, fine surface, or paint display effect, photosensitive resin, CNC plastic, or additional post-treatment should be considered.

Already have the blueprints? Directly enter the quotation for custom parts

After uploading 3D/2D drawings and supplementing materials, quantities, tolerances, surface treatments, and delivery requirements, XPartsLab will provide next steps in 3D printing manufacturability, cost, and delivery pathways.