
Core advantages
Stable printing, moderate cost, rich color effects, distinct stripe appearance, suitable for model display, suitable for quick proofing, minimal shrinkage in molding, and easier to print than ABS.
FDM 3D printing materials suitable for appearance display, decorative models, cultural and creative products, rapid prototyping, and low-strength structural validation.
PLA Filament is a PLA-like plastic material used for FDM/FFF melt deposition 3D printing, typically achieving striped visual effects through multicolor, gradient, or texturized filaments. It retains the characteristics of PLA material such as easy printing, stable molding, relatively clean surface, and moderate cost, while also offering more pronounced decorative and visual recognition. It is suitable for making display models, cultural and creative products, decorative parts, teaching models, consumer product appearance samples, and low-strength structural verification parts.
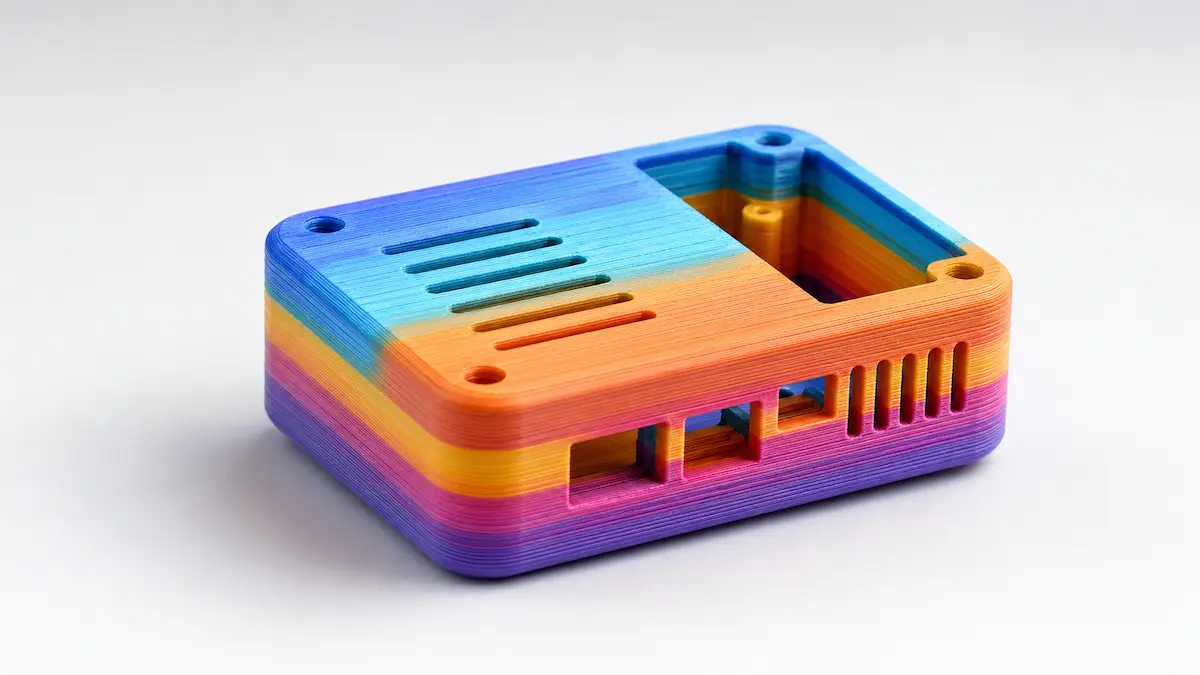
By focusing on application scenarios, boundaries of advantages, and non-recommended scenarios, it helps sales, customer service, and quoting staff quickly determine whether the material meets current part requirements.
Stable printing, moderate cost, rich color effects, distinct stripe appearance, suitable for model display, suitable for quick proofing, minimal shrinkage in molding, and easier to print than ABS.
Display models, cultural and creative ornaments, decorative parts, educational models, toy models, consumer product appearance samples, art models, low-strength shell samples, proof-of-concept models, non-load-bearing structural components, and small-batch display pieces.
Long-term load-bearing parts, high-temperature use parts, outdoor long-term use parts, high-impact parts, high-toughness snap fasteners, high-strength threaded parts, long-term immersion parts, wear-resistant moving parts, food direct contact parts, high-precision assembly functional parts.
The following parameters come from product information and material knowledge fields, used for design review, quotation communication, and preliminary judgment before material selection.
| Material positioning | FDM 3D printing materials suitable for appearance display, decorative models, cultural and creative products, rapid prototyping, and low-strength structural validation. |
|---|---|
| Precision performance | PLA Filament generally has good print stability, suitable for ordinary appearance models and low-strength structural verification. Actual accuracy is affected by equipment precision, nozzle diameter, layer height, printing direction, cooling conditions, model size, and post-processing methods. Compared to photosensitive resin, FDM printed surface textures are more pronounced, with lower detail sharpness. |
| Dimensional tolerances | Standard dimensional tolerances can refer to ± 0.20mm to ±0.50mm. This value is the FDM process reference value and does not guarantee absolute tolerances for all structures. Small, simple parts are usually more stable, while large-sized parts, thin-walled parts, slender parts, and complex structural parts may experience greater dimensional deviations. It is recommended to leave a margin for precision assembly positions, and if necessary, post-processing or trial assembly adjustments. |
| Minimum Wall Thickness | It is recommended that the wall thickness be no less than 1.0mm. Since FDM is usually formed according to the nozzle width and outer wall line width, it is recommended to design at least 2-3 outer walls for ordinary exterior parts. Small, non-stressed local structures can be close to 0.8mm, but are not recommended for large-area use. |
| Recommended wall thickness | For ordinary exterior parts, 1.2mm-2.0mm is recommended; for low-strength structural parts, 2.0mm or more is recommended; for parts requiring screw connections, assembly, or transport protection, 2.0mm-3.0mm is recommended. Strength should be enhanced by combining fill rate and rib design. |
| Minimum aperture | It is recommended that the aperture diameter be no less than 1.5mm. FDM small holes tend to shrink due to extrusion expansion, layering, and cooling shrinkage, so the actual formed round holes may not be round enough. It is recommended to reserve extra space for precision holes, screw holes, and positioning holes; if necessary, drill or enlarge holes after printing. |
| Assembly clearance | For ordinary assembly, it is recommended to reserve 0.20mm-0.40mm on one side; for movable fitting, 0.40mm-0.60mm should be reserved on one side; if painting or post-treatment is needed, an additional gap of about 0.10mm-0.20mm per side should be added. For clips, slides, and plug-in structures, evaluation should be conducted separately in conjunction with printing direction and interlayer strength. |
| Detailed performance | Raised text, fine textures, and decorative lines are recommended to be no less than 0.6mm-1.0mm. FDM printing detail performance is greatly affected by nozzle diameter and layer height; text and textures that are too small are easily unclear. The striped material itself has noticeable color changes, which may weaken the visual recognition of fine text and light textures. |
| Surface effect | The original surface features the layered patterns commonly seen in FDM printing, while also presenting stripes, gradients, or multicolor visual effects. The striped effect is suitable for decoration and display, but its surface texture is not as fine as photosensitive resin or CNC machined parts. By lowering the shelf, optimizing print direction, and adjusting exterior wall parameters, surface consistency and visual effects can be improved. |
Based on material characteristics and suitable product ranges, customer needs are broken down into easier application directions to determine.
Display models, cultural and creative ornaments, decorative parts, educational models, toy models, consumer product appearance samples, art models, low-strength shell samples, proof-of-concept models, non-load-bearing structural components, and small-batch display pieces.
FDM 3D printing materials suitable for appearance display, decorative models, cultural and creative products, rapid prototyping, and low-strength structural validation.
The main feature of PLA Filament material is that after printing, it has striped, gradient, or multicolor visual effects, making it more suitable for display and decorative applications than ordinary monochrome PLA. It is easy to print and has a low risk of warping, making it suitable for quickly creating appearance models and creative products. However, the overall temperature resistance, toughness, and impact resistance of PLA are limited, making it unsuitable for long-term use as high-strength functional components.
Based on wall thickness, hole position, assembly clearance, dimensional tolerances, and material usage risks, determine in advance whether the part structure is suitable for PLA Filament.
Post-processing of PLA Filament affects appearance, dimensions, hole position, assembly clearance, and usage validation results, and should be explained in advance during quotation, DFM review, and sample confirmation stages.
Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.
For common issues such as threads, snaps, strength, temperature resistance, and weather resistance, identify in advance whether the material needs to be replaced or if another processing method should be used.
When customer demand exceeds PLA Filament material boundaries, it is necessary to combine strength, temperature resistance, toughness, long-term stability, and mass production goals to promptly recommend alternative materials or processing technologies.
If better toughness and impact resistance are needed, PETG can be chosen; If higher temperature resistance and engineering performance are required, ABS, ASA, Polycarbonate (PC), or nylon can be chosen; If a finer appearance is required, photosensitive resin can be chosen; If more realistic mass-produced plastic performance is needed, CNC ABS, CNC Polycarbonate (PC), or injection molding materials can be chosen; If you only need ordinary, low-cost prototyping, you can choose standard PLA.
If customers mainly focus on appearance display, color effects, quick prototyping, and low-cost model production, PLA Filament is a more suitable choice. If customers need long-term force exposure, high temperature resistance, impact resistance, outdoor use, or performance close to mass-produced functional parts, priority should be given to PETG, ABS, ASA, nylon, CNC plastic, or metal processing.
After uploading 3D/2D drawings and supplementing materials, quantities, tolerances, surface treatments, and delivery requirements, XPartsLab will provide next steps in 3D printing manufacturability, cost, and delivery pathways.