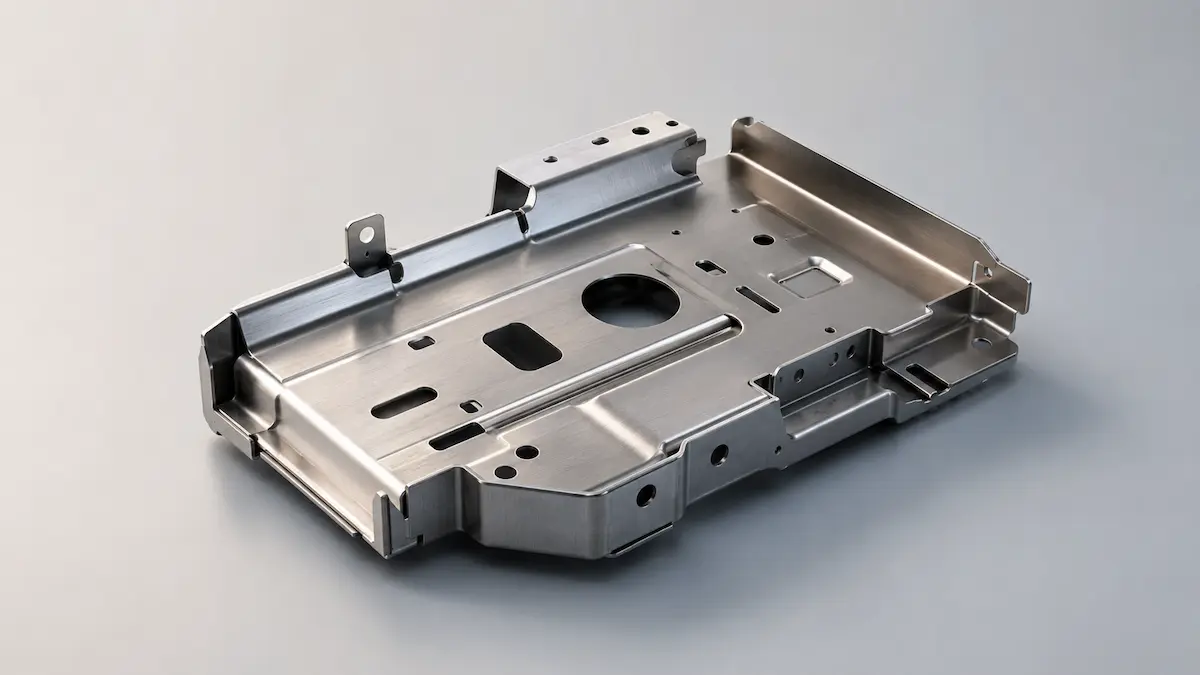
Post-processing options
Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.
Remove burrsDeburring is used to improve the appearance of parts, assembly, or functional verification effects, and it is necessary to confirm the impact on dimensions, strength, and delivery in combination with material characteristics.
ChamferChamfering is used to improve the appearance of parts, assembly, or functional verification effects, and the dimensions, strength, and delivery impact need to be confirmed in combination with material characteristics.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
BrushedBrushing is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
PolishingUsed to improve transparency or surface smoothness, may change edge details and local dimensions.
Mirror polishingMirror polishing is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties to confirm dimensions, strength, and delivery impact.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
PassivationCommonly used for corrosion-resistant treatment of stainless steel, it is necessary to confirm treatment requirements based on surface condition and usage environment.
Key control point
Size impactSUS201 can be brushed; Polishing and sandblasting; However, after surface treatment, rust prevention and cleaning maintenance are still necessary; Oxidation and discoloration may occur in the welded area; Reduced weld spot and corrosion resistance; Appearance parts need to be polished; Pickling; passivation or cleaning treatment
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.