Support Hours: 09:00–18:00 (GMT+8) · Messages and quote requests are accepted 24/7.
Material Database

TA2 Commercially Pure Titanium

Industrial pure titanium materials suitable for corrosion-resistant parts, lightweight metal parts, medical device parts, chemical equipment parts, marine environment parts, high-end consumer product parts, and medium-strength titanium metal structural parts.

Material description

Pure titanium TA2 is an industrial pure titanium material characterized by low density, good corrosion resistance, good biocompatibility, moderate strength, and a premium metallic texture. It is commonly used in medical devices, chemical equipment, marine environmental components, aerospace non-high-strength structural components, corrosion-resistant connectors, precision structural components, and high-end consumer product parts. Compared to TC4 Titanium Alloy (Ti-6Al-4V), TA2 has lower strength but generally better formability, weldability, and corrosion resistance; Compared to stainless steel, TA2 is lighter and has better corrosion resistance, but its processing cost is higher.

TA2 pure titaniumIndustrial pure titanium TA2Pure titaniumGrade 2 TitaniumTitanium Grade 2Grade II pure titaniumTitanium material TA2Medical-grade pure titaniumCorrosion-resistant titanium material
The core characteristic of pure titanium TA2 is its excellent corrosion resistanceLightweight and highly stable overallEspecially suitable for humid conditionsSeawaterWeak acidity and alkalinityChemical media and scenarios requiring biocompatibilityTA2 has a strength higher than that of ordinary plastics and most aluminum alloys in low-strength statesBut it is lower than TC4 Titanium Alloy (Ti-6Al-4V) and high-strength steelIt is more difficult to process than aluminum alloys and ordinary stainless steelHeat is easily generated during the cutting process
TA2 Commercially Pure Titanium
CNC MachiningMetals

Material compatibility assessment

By focusing on application scenarios, boundaries of advantages, and non-recommended scenarios, it helps sales, customer service, and quoting staff quickly determine whether the material meets current part requirements.

Core advantages

Lightweight, good corrosion resistance, good biocompatibility, good weldability, formability superior to most titanium alloys, premium metallic texture, suitable for humid and corrosive environments, suitable for long-term use, lighter than stainless steel.

Suitable for the product

Medical device parts, dental-related samples, surgical tool non-implantable structural parts, chemical equipment parts, corrosion-resistant pipe joints, marine environment parts, lightweight structural parts, precision brackets, high-end consumer product housings, sports equipment accessories, watch accessories, drone non-heavy-duty structural parts, laboratory equipment parts, corrosion-resistant fasteners.

Not suitable for the product

Ultra-high strength load-bearing parts, high-hardness wear-resistant parts, high conductivity parts, high thermal conductivity parts, high elasticity snap-fit parts, low-cost ordinary structural parts, large-size low-budget parts, high-speed friction moving parts, cost-sensitive parts for processing, and structural parts requiring the highest strength titanium alloy performance.

Key parameter references

The following parameters come from product information and material knowledge fields, used for design review, quotation communication, and preliminary judgment before material selection.

Material positioningIndustrial pure titanium materials suitable for corrosion-resistant parts, lightweight metal parts, medical device parts, chemical equipment parts, marine environment parts, high-end consumer product parts, and medium-strength titanium metal structural parts.
Precision performancePure titanium TA2 is suitable for CNC turning, milling, drilling, tapping, wire cutting, and precision machining. CNC machining can achieve better dimensional accuracy and assembly surface quality, but it is more difficult to process than aluminum alloys and ordinary steel. Actual accuracy is affected by part dimensions, wall thickness, clamping method, cutting tools, machining heat, material springback, and post-processing. Thin-walled parts, deep cavity parts, small holes, and thread positions require focused control of machining risks.
Dimensional tolerancesThe conventional dimensional tolerances for CNC-machined pure titanium TA2 can be referenced ± 0.02mm to ±0.10mm, while ordinary structural parts can be evaluated at ± 0.10mm to ±0.20mm. Thin-walled parts, large parts, complex curved surfaces, deep holes, and post-processing parts may experience greater deviations. These values are standard reference ranges and do not guarantee absolute tolerances for all structures. It is recommended to mark tolerance requirements separately for precision assembly surfaces, threaded holes, and positioning holes.
Minimum Wall ThicknessThe wall thickness of ordinary CNC machined structures is recommended to be no less than 0.8mm-1.0mm. Small non-stressed local structures can be further optimized according to machining capacity, but large-area over-thin areas are not recommended. Due to the high risk of heat and clamping deformation during titanium processing, thin-walled parts, long-conditioned parts, and large flat parts require special evaluation of processing deformation.
Recommended wall thicknessFor ordinary structural parts, 1.5mm-3.0mm is recommended; for load-bearing brackets, mounting seats, screw posts, clamping positions, and positions requiring post-processing, it is recommended to be at least 2.0mm; for thin-shell parts, rigidity is improved through reinforcing ribs, rounded corners, and local thickening to avoid machining and assembly deformation.
Minimum apertureCNC machining can achieve smaller hole diameters, but titanium materials are more difficult to machine with deep small holes, requiring higher chip removal and heat dissipation. Standard designs recommend hole diameters not less than 1.0mm; deep holes, small threaded holes, and high-precision positioning holes should be evaluated in conjunction with tool length, cooling, chip evacuation, and machinability assessment. For precision holes and threaded holes, it is recommended to use drilling, reaming, tapping, or post-processing to ensure dimensions.
Assembly clearanceFor precision metal assembly, one side can be reserved at 0.02mm-0.10mm according to fitting requirements; for ordinary plug-in and assembly, it is recommended to reserve 0.10mm-0.30mm per side. If subsequent surface treatments such as sandblasting, polishing, anodizing, micro-arc oxidation, or other surface treatments are required, additional gaps should be reserved according to changes in surface thickness and roughness. Attention should be paid to preventing seizure between titanium threads and sliding fits.
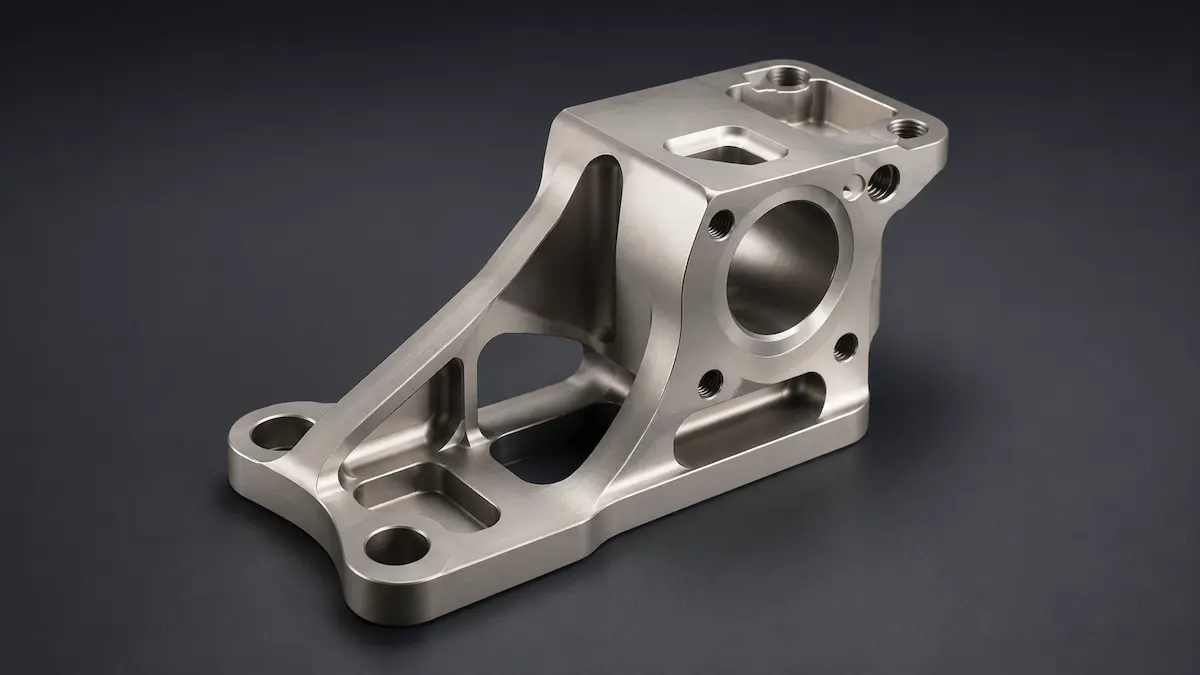
Detailed performancePure titanium TA2 is suitable for machining holes, grooves, steps, chamfers, threads, curved surfaces, brushed textures, sandblasted appearances, and precise structural details. CNC machining details are relatively good, but too small details, deep narrow grooves, small threads, and thin edges increase machining difficulty and cost. Small text, logos, and markings are recommended to be achieved through laser marking, engraving, etching, or anodizing for color difference.
Surface effectThe original machined surface of pure titanium TA2 is usually silver-gray or light gray metallic, giving it a higher-grade titanium appearance. After sandblasting, a uniform matte gray effect is achieved; brushing produces a delicate linear texture; polishing produces a brighter metallic surface; and anodizing produces decorative colors such as blue, purple, and gold. Titanium has a good appearance and texture, but surface scratches and processing textures require careful control.

Typical application scenarios

Based on material characteristics and suitable product ranges, customer needs are broken down into easier application directions to determine.

Product validation

Medical device parts, dental-related samples, surgical tool non-implantable structural parts, chemical equipment parts, corrosion-resistant pipe joints, marine environment parts, lightweight structural parts, precision brackets, high-end consumer product housings, sports equipment accessories, watch accessories, drone non-heavy-duty structural parts, laboratory equipment parts, corrosion-resistant fasteners.

Reasons for material selection

Industrial pure titanium materials suitable for corrosion-resistant parts, lightweight metal parts, medical device parts, chemical equipment parts, marine environment parts, high-end consumer product parts, and medium-strength titanium metal structural parts.

Material characteristics

The core features of pure titanium TA2 are excellent corrosion resistance, light weight, and strong overall stability, making it especially suitable for environments with humidity, seawater, weak acids and alkalis, chemical media, and biocompatibility requirements. TA2 has higher strength than ordinary plastics and most aluminum alloys in low-strength states, but is lower than TC4 Titanium Alloy (Ti-6Al-4V) and high-strength steel. It is more difficult to process than aluminum alloys and ordinary stainless steel, and during cutting it can easily generate heat, stick stick, and tool wear, resulting in higher machining costs.

Design and risk review

Based on wall thickness, hole position, assembly clearance, dimensional tolerances, and material usage risks, determine in advance whether the part structure is suitable for TA2 Commercially Pure Titanium.

Design considerations

  • When designing pure titanium TA2 parts,
  • Avoid overly deep and narrow grooves
  • Pass the small inner R corner
  • passing by the long, thin wall
  • Sharp internal corners and structures that are difficult to clamp in
  • It is recommended to add fillets and transition structures to the load-bearing positions
  • Avoid stress concentration
  • Threaded holes
Precision performancePure titanium TA2 is suitable for CNC turning, milling, drilling, tapping, wire cutting, and precision machining. CNC machining can achieve better dimensional accuracy and assembly surface quality, but it is more difficult to process than aluminum alloys and ordinary steel. Actual accuracy is affected by part dimensions, wall thickness, clamping method, cutting tools, machining heat, material springback, and post-processing. Thin-walled parts, deep cavity parts, small holes, and thread positions require focused control of machining risks.
Dimensional tolerancesThe conventional dimensional tolerances for CNC-machined pure titanium TA2 can be referenced ± 0.02mm to ±0.10mm, while ordinary structural parts can be evaluated at ± 0.10mm to ±0.20mm. Thin-walled parts, large parts, complex curved surfaces, deep holes, and post-processing parts may experience greater deviations. These values are standard reference ranges and do not guarantee absolute tolerances for all structures. It is recommended to mark tolerance requirements separately for precision assembly surfaces, threaded holes, and positioning holes.
Quality riskThe main risks of pure titanium TA2 are high processing costs, difficult cutting, easy surface scratches, thin-wall processing deformation, thread engagement, performance changes in the heat-affected zone, and color differences in surface treatment. It has excellent corrosion resistance, but does not guarantee stability in all strong acid, strong alkali, or high-temperature corrosive environments. For medical, chemical, marine, or long-term service scenarios, confirmation should be made based on the specific medium, temperature, load, and surface treatment.
Surface effectThe original machined surface of pure titanium TA2 is usually silver-gray or light gray metallic, giving it a higher-grade titanium appearance. After sandblasting, a uniform matte gray effect is achieved; brushing produces a delicate linear texture; polishing produces a brighter metallic surface; and anodizing produces decorative colors such as blue, purple, and gold. Titanium has a good appearance and texture, but surface scratches and processing textures require careful control.

Post-processing and assembly precautions

Post-processing of TA2 Commercially Pure Titanium affects appearance, dimensions, hole position, assembly clearance, and usage validation results, and should be explained in advance during quotation, DFM review, and sample confirmation stages.

Post-processing options

Post-processing should focus on appearance display, dimensional fitting, connection assembly, and testing verification. Parts involving assembly positions need to be reserved in advance for machining, coating, and trial assembly allowances.

Remove burrsDeburring is used to improve the appearance of parts, assembly, or functional verification effects, and it is necessary to confirm the impact on dimensions, strength, and delivery in combination with material characteristics.
PolishingImproves support marks, layer lines, and edge feel, but will slightly alter local dimensions and the shape of sharp edges.
SandblastingAchieve a more uniform matte surface, suitable for engineering prototype display and slight surface mark reduction.
PolishingUsed to improve transparency or surface smoothness, may change edge details and local dimensions.
BrushedBrushing is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
AnodizingSuitable for aluminum alloy appearance and protective treatment, pay attention to the impact of film thickness on hole position and assembly surface.
Micro-arc oxidationMicro-arc oxidation is used to improve the appearance, assembly, or validation of parts, and must be combined with material properties to confirm dimensions, strength, and delivery impact.
PicklingPickling is used to improve the appearance, assembly, or validation of parts, and must be determined by combining material properties with dimensions, strength, and delivery impact.

Key control point

Size impactWhen processing pure titanium TA2, attention should be paid to tool wear; Processing heat; Knife sticking and surface scratches; polishing; Polishing and sandblasting alter surface roughness and local dimensions; Anodizing and micro-arc oxidation can produce special colored or functional film layers; However, color consistency is affected by surface conditions; Titanium threads and assembly surfaces need to avoid interlocking
Assembly clearanceFor positions involving snapping, plugging, sliding, or enclosure closure, the clearance needs to be adjusted according to post-processing thickness, material shrinkage, and trial assembly results.
Hole Position StrengthThreading, inserting nuts, locking screws, and the areas around positioning holes need to ensure wall thickness to avoid cracks, stripped threads, or chipped edges during post-processing or assembly.
Environmental matchingWhen used in high-temperature, outdoor, humid, friction, or load-bearing scenarios, post-processing materials, adhesives, coatings, and fasteners must also meet the corresponding usage environment.

Structure and usage boundaries

For common issues such as threads, snaps, strength, temperature resistance, and weather resistance, identify in advance whether the material needs to be replaced or if another processing method should be used.

Thread Recommendation

Applicable ScopePure titanium TA2 can be used for tapping and thread processing, but titanium threads are prone to sticking and wear.
Risk pointFor frequent disassembly, high locking force, or highly reliable connection positions, it is recommended to increase the thread meshing length, use anti-sepress lubrication, sleeves, standard fasteners, or properly matched materials.
Recommended practiceSmall threads and deep threads are difficult to machine and should reserve enough machining space and margins.

Buckle recommendation

Applicable ScopePure titanium TA2 is not suitable for large deformation elastic buckles like plastic.
Risk pointDesigns can include low-deformation metal slots, pressure plates, pin connections, screw fixation, bending and snapping, or low-deformation spring structures, but evaluation must be based on titanium elasticity, fatigue life, plate thickness, and processing methods.
Recommended practiceWhen high-elasticity snap-fit is needed, spring steel, 301 stainless steel, beryllium copper, or engineering plastic snap-fit solutions should be considered.

Strength and Environment

Mechanical strengthPure titanium TA2 has moderate strength, significantly higher than most plastic materials but lower than TC4 Titanium Alloy (Ti-6Al-4V) and high-strength steels.
Environmental boundaryIt has good plasticity, toughness, and corrosion resistance, making it suitable for medium-strength lightweight structural components and corrosion-resistant functional parts.
Recommended practiceIf parts require high strength load-bearing, high impact, or high fatigue performance, priority should be given to TC4 Titanium Alloy (Ti-6Al-4V), alloy steel, or high-strength stainless steel materials. Pure titanium TA2 has better temperature resistance than plastics, resins, and most ordinary aluminum alloy applications, making it suitable for metal structures and corrosion-resistant applications at certain temperatures. However, TA2 is not a specialized high-temperature alloy, so its strength, oxidation state, and surface properties may change over long-term high-temperature conditions. When high-temperature load-bearing, thermal cycling, strong oxidation, or corrosive media are involved, verification should be conducted in consideration of specific temperature, load, and usage environment. Pure titanium TA2 has excellent corrosion and weather resistance, and is stable in humid conditions, seawater, sweat, weak acids and alkalis, and most natural environments, making it less prone to rust like carbon steel. Its surface forms a stable passivation film, which is beneficial for long-term use. However, when using special highly corrosive media, high-temperature corrosive environments, or contact with distinct metals, electrochemical corrosion, media adaptation, and surface treatment solutions must still be considered.

Alternative material selection and final judgment

When customer demand exceeds TA2 Commercially Pure Titanium material boundaries, it is necessary to combine strength, temperature resistance, toughness, long-term stability, and mass production goals to promptly recommend alternative materials or processing technologies.

Alternative material suggestions

If higher strength and better load-bearing performance are required, TC4 Titanium Alloy (Ti-6Al-4V) can be chosen; If lower cost and standard corrosion resistance are needed,304 Stainless Steel or 316L can be chosen; If lightweight and cost-effective is needed,6061 Aluminum Alloy or 7075 are options; If high thermal or electrical conductivity is required, Pure CopperT2, TU2 Oxygen-Free Copper, or aluminum alloys can be chosen; If only appearance verification is needed, photosensitive resin, nylon, or aluminum alloy sandblasted oxide parts can be chosen.

Material selection suggestions

If customers care about lightweight design, corrosion resistance, biocompatibility, long-term stability, and high-end metallic texture, pure titanium TA2 is a more suitable choice. If customers are more concerned about high-strength structural performance, TC4 Titanium Alloy (Ti-6Al-4V) should be prioritized; If customers care more about cost and standard structural processing, stainless steel or aluminum alloys are usually more economical; If customers require high thermal conductivity, high electrical conductivity, or high wear resistance, TA2 is usually not the preferred material.

Already have the blueprints? Directly enter the quotation for custom parts

After uploading 3D/2D drawings and supplementing materials, quantities, tolerances, surface treatments, and delivery requirements, XPartsLab will provide next steps in 3D printing manufacturability, cost, and delivery pathways.